
Contents
- Three Bending Methods, Three Different Tooling Demands
- How the Tooling Works in Each Method
- The Three Methods Side by Side
- How to Select: Three Steps
- Springback: Three Methods, Three Behaviours
- Machine Type Decides Which Method Is Even Possible
- Five Tooling Mistakes That Cost the Most
- What to Choose Comes Down to Three Constraints
- Frequently Asked Questions
The bending method is not a shop preference. It is where tooling selection starts. The same 90° part needs a different set of tooling for air bending, for bottoming and for coining: the geometry, the contact area, the wear rate and the precision requirement all change with it.
Most shops learn one bending method and then run every job with the same V die. The result is unstable angles and heavy springback, or premature tooling failure, or both. The reason is simple: the three methods place incompatible demands on the punch and the die.
This article takes the three methods apart one at a time: how the tooling works in each, what it demands, how to select it, how to manage springback, how the machine type changes the picture, and the five mistakes that cause the most rework. The figures in the tables are the shared rules of the craft and are safe to calculate from, but they are a starting point rather than a conclusion.
If you are choosing a V value for a new die right now, two companion articles on the site cover it: one on choosing a V die, one on sizing a V opening, with three worked examples.
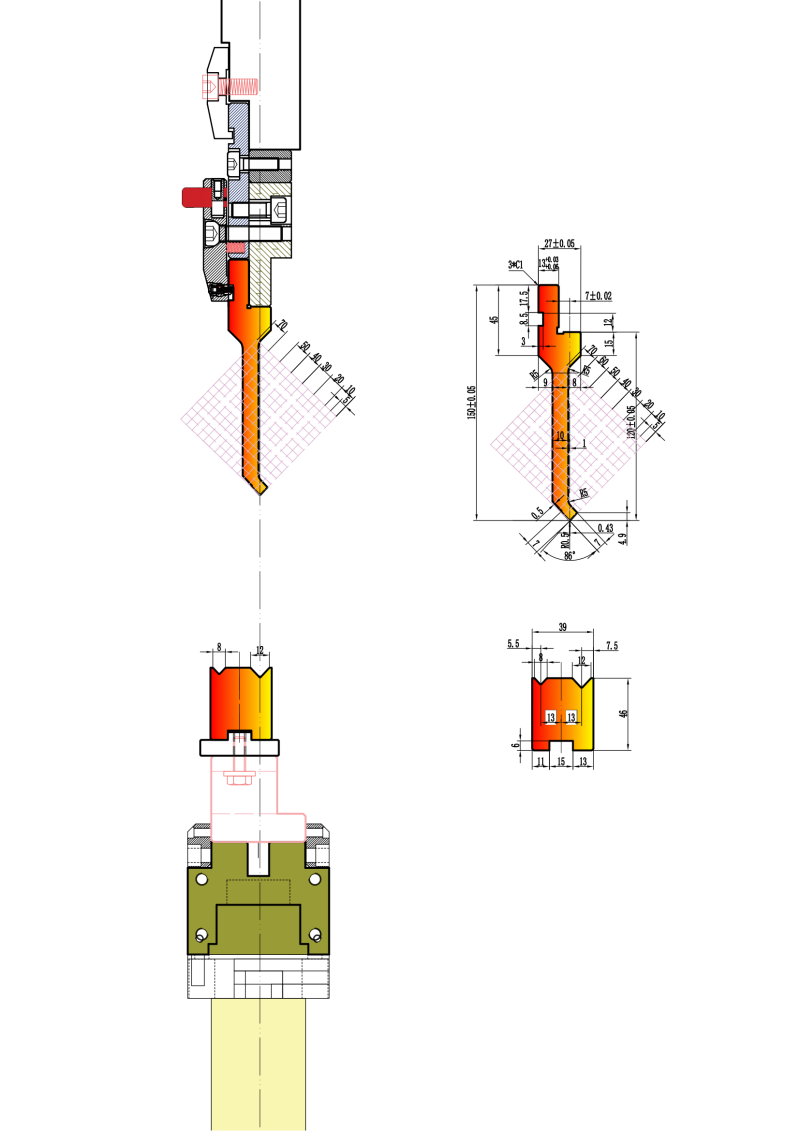
1. Three Bending Methods, Three Different Tooling Demands
Air bending tooling is the most versatile: one die handles a range of angles. Bottoming needs matched tooling per angle, and delivers tighter consistency. Coining demands the highest tonnage and wears the tooling fastest. Die opening width is the single variable that drives inside radius and required force. Springback behaves differently in all three, and so does the compensation.
- Air bending tooling is the most versatile: one die handles a range of angles.
- Bottoming needs matched tooling per angle, and delivers tighter consistency.
- Coining demands the highest tonnage and wears the tooling fastest.
- Die opening width is the single variable that drives inside radius and required force.
- Springback behaves differently in all three, and so does the compensation.
2. How the Tooling Works in Each Method
In air bending the sheet contacts the tooling at three points only: the punch tip and both shoulders of the die. The metal never touches the bottom of the die, and a gap of air is left between them. That gap is where the name comes from.
The bend angle is set by how far the punch descends, not by the shape of the die. The same set of tooling therefore produces a range of angles simply by changing the stroke depth. That is the practical value of air bending: one die, a batch of different angles.
In bottoming the punch drives the sheet all the way into the die until it touches the punch tip and the die sidewalls at the same time. The metal follows the tooling more closely and the angle comes out more precise, at the price of one dedicated die per target angle.
Coining applies extreme tonnage, typically ten times that of air bending on the same material, and compresses the sheet fully between punch and die. The bend zone thins slightly, and the angle is set entirely by the tooling geometry. It is the most accurate method and the most demanding on both the machine and the tooling.
2.1 Air Bending Tooling
A standard V die is enough. No custom tooling is required.
The punch tip radius should be at least 0.63 times the material thickness, which spreads the stress and reduces the risk of cracking.
The die opening is typically eight times the material thickness, which gives the most even force distribution.
The contact area is small, so the tooling wears slowly. That is the most practical advantage of air bending on cost.
2.2 Bottoming Tooling
Angle-specific dies are required: an 88° die makes a 90° part once springback has carried it there.
The tooling investment is larger and changeover takes longer. That is the main cost of the approach.
The contact area is medium and so is the wear.
The higher pressure can leave marks on the part surface.
2.3 Coining Tooling
The punch and the die must be matched exactly to the target angle, not approximately but precisely.
The contact area is the largest and the stress and wear on the tooling are the highest, so regular inspection is required.
Springback is essentially eliminated, so no overbending compensation is needed. That is the most practical benefit of coining.
The tooling has to be designed for coining; a standard V die will not do.
3. The Three Methods Side by Side
Here is the choice compressed into one table, to compare against when the decision is actually being made. Every row is a real technical difference rather than a sales argument.
| Criterion | Air bending | Bottoming | Coining |
|---|---|---|---|
| Tooling versatility | High — one die, many angles | Low — one die per angle | Low — exact match required |
| Angle accuracy | ±1° | ±0.5° | Better than ±0.25° |
| Springback | High | Moderate | Near zero |
| Tonnage required | Low (1×) | Medium (5×) | High (10×+) |
| Tooling wear | Low | Medium | High |
| Surface marks | Minimal | Possible | Likely |
| Tooling cost | Low | Medium | High |
| Best for | Prototypes, varied angles | Precision production runs | Aerospace, tight tolerances |
4. How to Select: Three Steps
The first step is always the die opening, because it decides the inside radius, the required force and the tooling life all at once. The second is the punch tip radius, which decides surface quality and cracking risk. The third is the material, because its strength and ductility change the answers to the first two.
The three steps have an order and they cross-check each other. Skipping the first and picking a punch directly, or skipping the second and ordering material, will cost you later.
| Material | Recommended method | Notes |
|---|---|---|
| Mild steel | Air bending or bottoming | Standard tooling works well |
| Stainless steel | Air bending | Needs 1.5–2× the tonnage |
| Aluminium | Air bending | Hard aluminium cracks easily; use soft alloys |
| High-strength steel | Coining | High precision required |
| Copper | Bottoming or coining | Soft and ductile; precise tooling recommended |
4.1 Step 1: Die Width Against Material Thickness
The general rule is: die opening = 8 × material thickness, for air bending and for bottoming.
A wider opening gives a larger inside radius and a lower force requirement, but a blunter angle.
A narrower opening gives a sharper angle, but more force and more stress on the tooling.
Coining has no such formula. The die has to match both the punch profile and the target angle precisely.
4.2 Step 2: Punch Tip Radius Against the Application
Air bending: tip radius ≥ 0.63 × material thickness.
Bottoming: the tip has to match the inside radius you want.
Coining: the punch geometry must match the die angle exactly. Use a matched tooling set.
4.3 Step 3: The Material Decides the First Two
The springback tendency, the ductility and the strength limit of the material together decide whether a given angle can be held repeatably.
5. Springback: Three Methods, Three Behaviours
Springback is elastic recovery: once the bending load is released, the metal tries to return toward its original flat shape. How far it goes depends on the method and the tooling.
Air bending produces the most springback, so the operator has to overbend to compensate, typically 1–3° depending on material and thickness. A laser angle measurement system turns that compensation into a measured value instead of a feel.
Bottoming produces moderate springback, and the practice is to set the tooling angle slightly more acute than the target: an 88° die for a 90° part, letting springback supply the missing 2°.
Coining produces almost no springback. The high tonnage fully plastically deforms the material, so the elastic recovery is gone and no compensation is needed at all.
Those three numbers, 1–3°, 2° and zero, are where the accuracy gap between the methods comes from. Air bending saves tooling money and pays for it in angle consistency; coining pays in tonnage and tooling and buys angle accuracy.
6. Machine Type Decides Which Method Is Even Possible
Not every press brake suits every bending method. The drive and the control decide which method the machine can hold repeatably.
Hydraulic press brakes are the most versatile: with the right tooling, all three methods are available. It is the general-purpose answer.
Electric and servo press brakes have the most precise stroke control, which makes them excellent for air bending. They can bottom, but heavy coining does not suit them.
Mechanical press brakes match bottoming best, because the die geometry itself controls the angle. With enough rated tonnage they can coin as well.
Older machines are a different case: bottoming can use the die geometry to compensate for the machine’s own inaccuracy instead of relying on a precise stroke.
For the GWMT range specifically, WPA and WPD are CNC platforms with configurable axes, suited to complex profiles and varied production; WC67K is an NC-controlled hydraulic platform for straightforward bending and repeat jobs; EP is a compact all-electric platform built for fast response and quick changeover on smaller precision parts. Choosing the machine and choosing the bending method are two sides of the same decision: start from the parts you need to make, and work back to the machine and the tooling.
7. Five Tooling Mistakes That Cost the Most
These five come up most often on the shop floor, and they are also the ones most often skipped during troubleshooting.
- 1. The die width does not match the material thickness. Too narrow: excessive force, damaged tooling, possible cracking. Too wide: insufficient deformation, inaccurate angles.
- 2. The punch tip radius is ignored. A tip below 0.63 × material thickness concentrates the stress and raises the risk of cracking.
- 3. Air bending tooling is used for coining. A standard V die is not built for coining tonnage and will fail early.
- 4. Springback compensation is skipped in air bending. The result is an angle wider than intended — always factor the material springback in.
- 5. Tooling maintenance is neglected during coining. The contact stress is high and the wear fast, so deformation or surface damage changes the bend directly.
8. What to Choose Comes Down to Three Constraints
Whether you use air bending, bottoming or coining comes down to three things: the precision your parts demand, the material you are working with, and the equipment you have available.
Air bending gives you the best flexibility and the lowest cost. Bottoming delivers reliable precision across production runs. Coining gives the highest accuracy for critical, tight-tolerance parts, at the cost of higher tonnage and faster wear.
Two more articles on the site cover the tooling itself: one on choosing a V die, one on sizing a V opening. Used together with the method described here, they form a complete set.
9. Frequently Asked Questions
- Can the same tooling be used for air bending and bottoming?
Sometimes, with caveats. A standard V die used for air bending can bottom as long as the angle matches your target once springback is accounted for, but the higher tonnage of bottoming will accelerate wear on tooling that was not rated for it.
- How do I know which die width to use?
Start from the rule of eight: die opening = 8 × material thickness. Narrow it for a sharper angle, which costs force, and widen it for softer material to avoid cracking.
- Does coining require special equipment?
Yes. Coining needs markedly more tonnage, typically ten times that of air bending on the same material. Check the rated tonnage before you start, because the machine pays for a shortfall.
Technical references
Manufacturer references support process explanations; images illustrate selection topics, not an approved GWMT supply specification.