
Contents
- Chapter One: What a Press Brake Proportional Valve Actually Is
- Chapter Two: How the Proportional Valve Works
- Chapter Three: How Proportional Valves Control a Bending Cycle
- Chapter Four: Y1/Y2 Synchronization and How Proportional Valves Keep the Ram Parallel
- Chapter Five: Proportional Valve versus Servo Valve
- Chapter Six: Separating Proportional Valve Faults from Other Hydraulic Problems
- Chapter Seven: Selecting or Replacing a Proportional Valve
- Chapter Eight: Installation and Service Safety
- Frequently Asked Questions
- Chapter Ten: Conclusion
There is one component on a press brake that even experienced people are careful about drawing conclusions on. When the ram runs faster on the left than on the right, nine people out of ten will say the proportional valve has a problem. Get to the machine, open it up, and the valve is usually fine: the fault is somewhere else, and it only shows up as a synchronisation symptom.
The problem is that the term proportional valve is easy to oversimplify. It sounds like a switch that adjusts continuously. In reality it is one link in a control chain: the command leaves the CNC, passes through the driver, the solenoid and the spool, drives the hydraulic cylinder, and returns through position feedback to form one controlled ram movement. If any link in that chain fails, what the operator sees may be nothing more than uneven travel. The reverse is equally true: a proportional valve reporting perfect internal feedback does not mean the ram actually reached its target.
This guide is about closing that gap. It works through the proportional valve in ten sections: what the valve is, how an electrical signal becomes hydraulic flow step by step, what the valve opening is doing at each of the six phases of a bending cycle, how closed-loop Y1/Y2 synchronization keeps the ram parallel, where the real difference between proportional and servo valves lies, how to separate a valve fault from other system faults, which five groups of parameters a replacement has to match, and finally the question that matters most: is the ram safe once the power is off. All four tables are kept in directly usable form.
Every parameter, signal format and range in this article is kept as given. Where hydraulic safety is involved, the source qualifiers are preserved: anything that belongs in the machine manufacturer documentation stays there and is not replaced by this article.
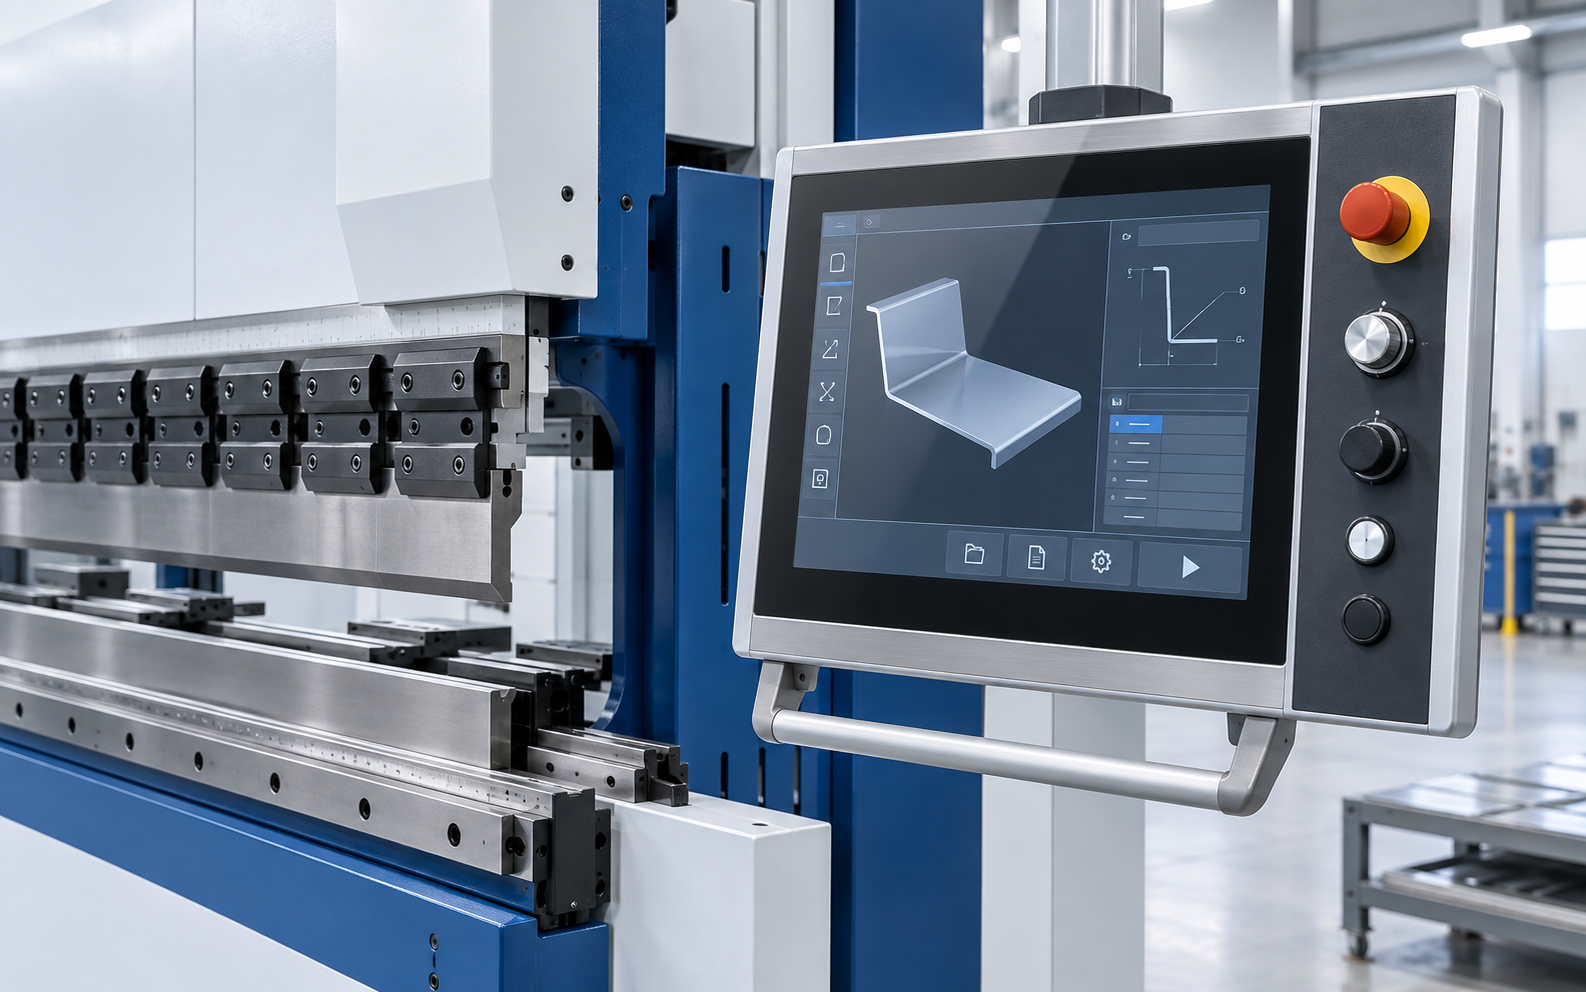
1. Chapter One: What a Press Brake Proportional Valve Actually Is
A proportional valve is an electrically controlled hydraulic valve that can hold any intermediate position within its range, not just fully open or fully closed. Its output changes continuously in response to the command signal, which is why one valve can meter a slow bending speed, hold a programmed pressure and release oil at a controlled rate during decompression, all within a single bending cycle.
The usual comparison, a proportional valve as a dimmer against a conventional on/off solenoid valve as a light switch, is accurate at the conceptual level. There is one important caveat: proportional does not mean perfectly linear. Actual hydraulic output also depends on the pressure difference across the metering edge, the flow the pump can deliver, oil temperature, valve deadband and load conditions. The valve is a controllable element in a larger system, not a standalone guarantee of ram accuracy.
On a press brake, proportional valves are normally organised by function.
- Proportional directional valves control which flow paths are active and meter how much oil moves in each direction, governing ram speed and movement direction
- Proportional pressure valves regulate the pressure threshold in part of the circuit, controlling the hydraulic force available to the cylinders
- Combined valve blocks integrate multiple functions into a manifold to reduce external plumbing and improve response
- These are different devices performing different roles. A single proportional valve does not simultaneously and independently control direction, speed and pressure. The hydraulic schematic, not the component name alone, shows what each valve actually does in a given machine.
2. Chapter Two: How the Proportional Valve Works
The valve converts an electrical command into a change in spool or poppet position, which alters how oil passes through the hydraulic circuit. The complete process involves four stages.
- Command and driver: the CNC or motion controller generates a variable command signal, commonly plus or minus 10 V, 0 to 10 V or 4 to 20 mA depending on the valve electronics. A valve driver, also called an amplifier, either external or integrated into the valve body as onboard electronics, converts that signal into regulated current through the solenoid coil.
- Solenoid and spool movement: coil current generates a magnetic force on the armature, which pushes the spool against spring and hydraulic forces. The spool shifts proportionally to the net force acting on it, changing the overlap between spool lands and port passages.
- Hydraulic metering: as the spool moves it progressively uncovers the connections between the pressure port, tank port and actuator ports. A larger opening generally allows more oil to pass, but only when the pressure difference across that opening and the pump available delivery support it. Hydraulic power, not the electrical command itself, moves the cylinders.
- Feedback and correction: some valves include an internal spool-position sensor that measures actual spool travel. The driver compares this measurement with the command and corrects the drive current until they match. This inner loop reduces the effect of mechanical friction and hysteresis on the valve metering behaviour.
2.1 2.1 Two Types of Hydraulic Actuation
That last point matters for troubleshooting: internal spool feedback corrects the valve element position. It does not confirm that the expected flow reached the cylinders, or that the ram followed its programmed target. Those require a separate, external measurement, which is what the linear scales on the machine provide.
- Direct-operated valves have the solenoid acting on the main spool itself. This is straightforward but limits practical flow capacity, because the solenoid must overcome the full hydraulic forces on the main spool.
- Pilot-operated valves use a small solenoid-driven pilot stage that directs oil into control chambers. The resulting pressure difference moves the larger main spool with relatively modest electromagnetic force, making this design suitable for higher-flow applications. The trade-off is an added dependency: the pilot circuit needs adequate supply pressure and a clear drain path. Low pilot pressure can prevent the main spool from reaching its commanded position even when the solenoid is energised correctly.
- This distinction is relevant for diagnosis: if a high-flow pilot-operated valve fails to respond, pilot supply conditions should be checked alongside the electrical command.
3. Chapter Three: How Proportional Valves Control a Bending Cycle
The valve role and the relevant hydraulic variables change at each stage of a bend. The sequence below follows a typical down-acting press brake; the exact circuit arrangement depends on the specific machine design.
- Rapid approach: the ram descends quickly. Depending on machine design, pump flow, gravity assistance or a prefill circuit supplies oil to the expanding cylinder chamber. Where a prefill valve is used it must operate correctly and transition cleanly as the circuit switches to bending pressure.
- Speed changeover: at the programmed position the CNC reduces the command to decelerate the ram before tool contact. This transition must happen before the tool reaches the workpiece; a delayed changeover transfers shock load to the tooling, the sheet and the machine structure.
- Bending: the tool contacts the material. Workpiece resistance builds pressure in the working cylinder chamber while the proportional valve meters controlled flow to continue penetration at the programmed rate. Rising pressure at this stage is a response to increasing load resistance, not a switch to a different control mode unless the program specifies pressure control.
- Bottom position or dwell: the ram holds at a programmed depth or pressure condition. In depth hold mode the target is a fixed position and pressure may change as the workpiece and machine settle. In pressure hold mode the target is a pressure value and minor ram movement may be permitted. Load-holding valves in the circuit retain the position with minimal continuous flow.
- Decompression: stored hydraulic energy and machine frame deflection are released progressively before the return begins. Skipping or rushing this stage causes hydraulic shock, audible bang and potential workpiece movement. A dedicated decompression valve, a proportional metering path, or both can perform this function.
- Return: pump flow enters the rod-side chamber to lift the ram. This stage requires pressure to overcome ram weight and friction; it is not passive. Oil leaving the cap-side chamber returns through the available discharge paths, which may include a reopened prefill valve on some machines.
4. Chapter Four: Y1/Y2 Synchronization and How Proportional Valves Keep the Ram Parallel
This is the function that most directly connects the press brake proportional valve to production accuracy. On an electro-hydraulic press brake the two hydraulic cylinders, labelled Y1 on the left and Y2 on the right, are controlled independently by separate proportional valves. Synchronization is achieved through closed-loop position control, not mechanical coupling.
The closed-loop process works like this.
- The CNC generates a target position at each point in the stroke.
- Linear scales on each side of the machine continuously measure actual cylinder position.
- The controller compares each measured position with the target and calculates a position error for Y1 and Y2 independently.
- It adjusts the command to each proportional valve to correct those errors, hundreds of times per second during the stroke.
4.1 4.1 Spool Position Feedback versus Ram Position Feedback
During an off-centre bend one cylinder carries more load and may lag slightly. The CNC detects this through the position error and applies a higher command to the lagging side. The result is that Y1 and Y2 commands are frequently different from each other, which is normal corrective action and not evidence of a valve fault.
- A valve with spool-position feedback uses an inner control loop to hold the spool at the commanded position more accurately. The machine outer loop, driven by linear scale data, corrects the overall ram position. Both loops run simultaneously on a well-configured electro-hydraulic machine, but they act on different parts of the system.
- A correctly positioned spool does not guarantee a correctly positioned ram. Leakage downstream of the valve, an incorrectly calibrated linear scale, or insufficient pump flow can all produce a ram-position error even when the valve internal feedback is working correctly.
| Feedback type | What it measures | What it cannot confirm |
|---|---|---|
| Spool position feedback, internal to the valve | Actual spool travel relative to the commanded position | Whether the expected flow reached the cylinders; whether the ram followed its target |
| Ram position feedback, external, from linear scales on the machine | Actual cylinder or ram displacement at the measurement point | Correct hydraulic pressure, bend angle, or tool penetration along the full bend length |
4.2 4.2 Electro-Hydraulic versus Torsion-Bar Synchronization
Torsion-bar synchronization connects the left and right sides of the ram mechanically through a steel shaft. The two sides are physically constrained to move together. This approach requires no electronic feedback and no proportional valve control, which keeps the machine simpler and less expensive. The limitation is that the bar cannot distinguish between correct coupling and an eccentric load forcing the bar to twist. Over time, sustained off-centre loading causes permanent deformation, and the resulting change in parallelism cannot be corrected automatically.
Electro-hydraulic synchronization replaces the mechanical link with electronic measurement and independent valve control. The CNC can detect a developing Y1/Y2 discrepancy within a single stroke and correct it before it becomes measurable at the workpiece. This makes the machine capable of handling off-centre loading that would impose sustained twisting on a torsion bar.
| Item | Torsion bar | Electro-hydraulic |
|---|---|---|
| Synchronization method | Mechanical steel shaft | Dual independent proportional valves with position feedback |
| Off-centre load handling | Limited; sustained eccentric loading damages the shaft | Handled through independent Y1/Y2 correction |
| Repositioning accuracy | Typically ±0.1 mm or greater | Typically ±0.01 mm or better |
| Self-correction over time | None | Continuous; adjusts every stroke |
| Typical application | Simpler, economy-tier press brakes | CNC electro-hydraulic press brakes for precision bending |
4.3 4.3 Why Proportional Valve Accuracy Does Not Equal Bend Angle Accuracy
Ram position accuracy and finished bend angle are related but not the same thing. Even with perfectly synchronised Y1 and Y2 positions, the unloaded workpiece angle depends on several factors.
- Material thickness and strength variation within a batch
- Springback, the partial elastic recovery after the ram retracts; different alloys and tempers spring back differently
- Tool geometry: punch radius, die opening and shoulder radius all influence the relationship between ram depth and finished angle
- Machine frame deflection under bending load, which changes effective tool penetration near the centre of a long bend relative to the ends
- Crowning, bed compensation for frame deflection, which operates independently of Y1/Y2 synchronisation
5. Chapter Five: Proportional Valve versus Servo Valve
The common framing, proportional valves for lower precision and servo valves for higher precision, is an oversimplification that can lead to incorrect specification decisions.
Both valve types provide continuously variable hydraulic control. The meaningful differences lie in the design parameters that govern dynamic behaviour.
- The key clarification: proportional valves can include internal spool-position feedback and operate as part of a closed-loop system. The difference between a modern proportional valve with OBE and a servo valve is therefore not simply open-loop against closed-loop. It is a difference in spool overlap, hysteresis, contamination tolerance and dynamic response at the design level.
- For the vast majority of production press brakes a well-specified proportional valve system delivers more than adequate performance. The practical argument for servo valves in a press brake context is a specific dynamic requirement or accuracy target that the proportional system cannot reliably meet, not a general assumption that servo is always better.
- When evaluating an electro-hydraulic press brake specification, ask specifically which valve brand and series is used, what the spool configuration is and whether the valve includes internal position feedback, rather than accepting servo proportional as a meaningful specification by itself.
| Characteristic | Proportional valve | Servo valve, high performance |
|---|---|---|
| Spool overlap | Positive overlap typical; produces a deadband around the null position | Zero or negative overlap typical; near-zero deadband |
| Response and bandwidth | Moderate; adequate for most industrial press brake cycles | Higher; suited to demanding fast closed-loop applications |
| Hysteresis | Present; reduced but not eliminated by electronics | Minimised by tighter manufacturing tolerances |
| Internal position feedback | Available on many current models, the OBE designs | Common; often the standard configuration |
| Contamination sensitivity | Tolerant of typical industrial cleanliness, ISO 4406 Class 16 to 18 typical | Requires stricter cleanliness, often Class 15 or better |
| Commissioning complexity | Moderate | Higher; tighter system design requirements |
| Typical press brake use | Ram speed control, Y1/Y2 synchronisation, pressure control | Specialised or very high-dynamic applications |
6. Chapter Six: Separating Proportional Valve Faults from Other Hydraulic Problems
The most useful troubleshooting principle: a proportional valve fault is a diagnosis of last resort, not a starting assumption. Most symptoms that appear to implicate the valve originate elsewhere in the electrical, hydraulic or mechanical system.
Before suspecting the valve, record the following.
- The exact alarm codes and their sequence
- The affected cycle stage: approach, changeover, bending, hold, decompression or return
- CNC display values: commanded against measured position for Y1 and Y2, and commanded against measured pressure where available
- Recent changes: oil, filters, sensors, tooling, parameter adjustments
- Oil temperature at the time of the fault
- Do not run repeated cycles or change parameters to gather additional evidence. Preserve the fault record for qualified service review.
6.1 6.1 How to Separate Valve Faults from System Faults
The following framework helps assign a symptom to the correct system layer before any hardware is touched.
- Step one, check the electrical command first: measure the command signal at the valve connector under the fault condition. If the command signal is absent or incorrect, the fault is upstream of the valve, so check the CNC output, driver module, wiring continuity, connector condition and enable logic. A valve cannot respond correctly to a signal it is not receiving.
- Step two, check hydraulic supply conditions: if the command signal is correct and the valve is energised, verify system pressure and filter status. Low supply pressure, a clogged filter or a restricted inlet line limits what any valve can deliver regardless of its condition. Many apparent valve faults resolve after a filter change or after confirming that the hydraulic pump is maintaining specified pressure at load.
- Step three, evaluate the symptom against the cycle stage: a fault appearing only during rapid approach points toward filling capacity, prefill valve behaviour or pump delivery, not proportional valve metering. A fault appearing only under bending load raises questions about pressure control, leakage under pressure and whether the cylinder can develop the required force. Drift during the hold stage points toward cylinder seal bypass, directional valve leakage or load-holding device condition, because the proportional valve is typically not responsible for holding load. Decompression shock or bang is almost always a decompression valve or sequence timing issue.
- Step four, distinguish valve sticking from valve failure: a proportional valve that was working and has degraded gradually usually shows contamination-related sticking, with sluggish or erratic response that is worse when the oil is cold and improves as the system warms up. This responds to oil and filter changes, sometimes to flushing the valve. A valve that fails abruptly, with no response or a total loss of a function, is more likely an electrical fault in the driver, wiring or connector than a mechanical failure of the spool.
| Symptom | Check first, before the valve | Valve-specific signs |
|---|---|---|
| No response | Command signal, enable circuit, driver power supply, wiring | Correct command present, driver energised, no mechanical response |
| Slow or sluggish movement | Filter condition, pump pressure, oil temperature, commanded speed setting | Correct command, adequate supply, still slow, and worse when cold |
| Jerking or hunting | Air in system, feedback signal noise, control tuning, cylinder seals | Stable command, no air, tuning unchanged, erratic valve movement on diagnostics |
| Uneven Y1/Y2 travel | Linear scale calibration, feedback wiring, differential cylinder leakage | Both scales confirmed accurate, leakage ruled out, commands diverging without load asymmetry |
| Ram drift during hold | Cylinder seal bypass, load-holding valve, directional valve leakage | Holding circuit confirmed tight, drift remains |
| Low bending force | Pump pressure setting, pressure-control valve, relief valve setting | Pressure command correct, pump at specification, force still insufficient |
6.2 6.2 What Causes a Proportional Valve to Fail
The most common causes in press brake service, roughly in order of frequency.
- Hydraulic contamination: particulate or water contamination causes spool sticking, accelerated bore wear and loss of metering precision. This is the leading cause of gradual performance degradation.
- Electrical driver fault: the driver, the amplifier, fails or drifts and delivers incorrect current to the solenoid coil. The valve spool is mechanically intact but receives wrong commands.
- Solenoid coil failure: coil burnout from overvoltage, incorrect supply or excessive continuous current. The spool will not move at all.
- Spool seizure: severe contamination or corrosion locks the spool mechanically. It is often preceded by a period of sluggish response.
- Feedback sensor failure on OBE valves: the internal spool-position sensor fails or drifts, causing the valve to command an incorrect spool position even with correct input signals.
- Wiring and connector degradation: intermittent faults from corroded connectors, damaged cables or signal interference. These are often temperature-dependent and difficult to reproduce consistently.
- A recurring valve fault that returns after replacement almost always has an underlying cause, usually contaminated oil, an incorrect driver setting or a wiring issue, that was not addressed before reinstalling the component.
7. Chapter Seven: Selecting or Replacing a Proportional Valve
Selecting a replacement requires matching the valve across five categories. A valve that fits the port and looks similar may still produce incorrect or unsafe machine behaviour if any of these parameters differ.
- Hydraulic function and rating: identify the valve function in the circuit, whether directional, pressure, flow or a combination within an integrated manifold, then confirm maximum working pressure, nominal and maximum flow rate, acceptable pressure drop at rated flow, and whether the design is direct-operated or pilot-operated.
- Electrical interface: this must match the machine drive system exactly, covering command signal type of plus or minus 10 V, 0 to 10 V, 4 to 20 mA or a digital interface such as IO-Link, supply voltage for the valve electronics, external amplifier or onboard electronics, internal spool-position feedback present or absent, connector specification and enable logic.
- Mechanical compatibility: mounting pattern and nominal valve size such as NG6, NG10 or NG16, port arrangement and manifold interface, seal material and hydraulic fluid compatibility, and operating temperature range.
- Fail-safe behaviour: confirm the defined spool rest position when power is removed, whether blocked ports, connection to tank or another configuration. The correct rest position is circuit-dependent, and a valve with the wrong fail-safe position can create unintended ram movement when the machine is shut down.
- For replacement on an existing machine, collect the complete nameplate code from the existing valve, machine manufacturer, model and serial number, CNC and hydraulic control system model, the relevant section of the hydraulic schematic, photographs of the installed valve, wiring and manifold connections, and a description of the fault and the operating conditions when it occurs.
- For obsolete valves where the original part is no longer available, the replacement selection must replicate the hydraulic function, spool configuration, pressure and flow capacity, command interface, mounting interface and fail-safe behaviour, not just the external dimensions and connector shape. Involve the machine manufacturer or a qualified hydraulic service specialist when working from an obsolete part number.
8. Chapter Eight: Installation and Service Safety
Proportional valve work on a press brake is a hydraulic service task with specific energy-isolation requirements. The hazards are not limited to electrical power.
A stopped pump does not eliminate stored hydraulic pressure. Oil can remain trapped under pressure in cylinders and isolated passages after the pump stops. A raised ram stores gravitational energy that can cause descent if a flow path opens or a seal bypasses. An accumulator, where fitted, retains hydraulic energy independently of the pump state.
Before any hands-on work:
- Follow the machine manufacturer written isolation procedure and applicable lockout and tagout requirements, covering electrical power, hydraulic pressure and ram weight.
- Use the manufacturer-specified mechanical ram support before working anywhere near the ram.
- Release hydraulic pressure through the prescribed procedure and verify depressurisation at the designated test points; do not assume a zero-pressure gauge reading means every passage is safe.
- If an accumulator is fitted, follow its separate discharge and verification procedure before disconnecting any lines.
- During installation, work from the machine hydraulic schematic and service manual. Confirm port identification, valve orientation, mounting torque, connector pinout and seal condition. The hydraulic circuit must be clean before the valve is installed, because contamination introduced during the procedure can damage the new component immediately.
- Do not bypass interlocks to observe valve behaviour under power. Do not loosen fittings on a pressurised circuit. Do not use a hand or fingers to locate hydraulic leaks; a pressurised jet can penetrate skin even when it is not visually obvious. Any energised testing or tuning requires qualified personnel following an approved procedure.
9. Frequently Asked Questions
The six questions below suit item-by-item confirmation with a customer, a colleague or a supplier.
- What does a press brake proportional valve do?
It converts a variable electrical command from the CNC into a proportional change in hydraulic flow, pressure or direction, allowing the machine to control ram speed, bending force and cylinder position continuously throughout the bending cycle rather than switching between fixed hydraulic states.
- Why is my press brake ram moving unevenly from side to side?
Uneven Y1/Y2 travel can result from a linear scale calibration error on one side, differential hydraulic leakage between cylinders, a flow restriction on one side of the circuit, or a control tuning issue. Check whether the position discrepancy appears on the CNC display only or is also physically observable, and compare Y1/Y2 commanded against measured values before attributing the fault to a proportional valve.
- What causes a proportional valve to fail?
The most common cause is hydraulic contamination leading to spool sticking and bore wear. Electrical failures, namely driver faults, coil burnout and connector degradation, are the next most frequent. Abrupt total loss of function usually points to an electrical cause; gradual performance degradation over time usually points to contamination. A valve that fails repeatedly after replacement almost always has an unresolved upstream cause.
- Can a proportional valve be replaced with a different model?
Only if the replacement matches the original across hydraulic function, spool configuration, pressure and flow rating, command signal type, mounting interface and fail-safe behaviour. Matching port size or connector shape is not sufficient. For obsolete part numbers, involve the machine manufacturer or a qualified hydraulic specialist to verify full functional compatibility.
- What is the practical difference between a proportional valve and a servo valve on a press brake?
The meaningful differences are spool overlap, which determines deadband, dynamic response bandwidth, hysteresis and contamination tolerance, not simply open-loop against closed-loop control, since many modern proportional valves include internal spool-position feedback. Servo valves are justified when the dynamic requirements of the application exceed what a proportional system can reliably deliver. Most production press brakes use proportional valves, which are adequate for industrial bending cycles and more tolerant of typical shop-floor hydraulic conditions.
- Is the press brake ram safe when the proportional valve is de-energised?
Not automatically. Most proportional valves return the spool to a defined rest position when power is removed, but whether the ram holds or descends depends on the hydraulic circuit design and the load-holding arrangement. Never rely on a de-energised valve, an emergency stop or a pump shutdown alone as mechanical protection when working near the ram. Follow the machine manufacturer lockout and ram-support procedure.
10. Chapter Ten: Conclusion
A press brake proportional valve is not a standalone precision device; it is one link in a control chain that runs from a CNC command through a valve driver, solenoid, spool, hydraulic cylinder and position feedback before producing controlled ram movement. Understanding each link in that chain determines how accurately a fault can be located and how a replacement can be correctly specified.
For maintenance and troubleshooting, the most productive starting point is identifying the affected cycle stage and comparing commanded against measured values on the CNC display before any hardware is changed. Most apparent valve faults originate in the electrical command path, hydraulic supply or feedback system.
For equipment evaluation, the proportional valve architecture, meaning closed-loop Y1/Y2 position control with independent cylinder correction, is what separates an electro-hydraulic CNC press brake from a mechanically synchronised machine in terms of synchronisation accuracy, off-centre load capability and long-term parallelism stability. When reviewing a machine specification, ask specifically about valve brand, series, spool configuration and whether internal position feedback is included; these details matter more than a generic servo proportional label.
If you are specifying an electro-hydraulic press brake for a new line, or trying to trace the root of a synchronisation question on existing equipment, the most useful questions are these: is Y1/Y2 synchronisation mechanical through a torsion bar or closed-loop electro-hydraulic, what does the ram position measurement rely on, and which valve brand and series is fitted with or without internal spool-position feedback. These three questions describe what the machine can actually do far better than any claim about accuracy class.
Technical references
Manufacturer references support process explanations; images illustrate selection topics, not an approved GWMT supply specification.