Frame and bed
Frame rigidity, bed envelope, access, and foundation planning are reviewed with the die and production duty.
A rigid-frame pneumatic press platform for repeat punching, blanking, forming, and compatible progressive-die production.
PRODUCT OVERVIEW
JH21 selection begins with the die, force curve, stroke, shut height, feeding method, guarding, and intended production duty. The whole press scope must be reviewed with the real tool and part.
MACHINE STRUCTURE
Frame rigidity, bed envelope, access, and foundation planning are reviewed with the die and production duty.
Slide travel, guide condition, and adjustment range are matched to the shut height, die envelope, and work sequence.
The drive, clutch/brake scope, and control method are selected with stroke pattern, cycle demand, and site operating procedure.
Die dimensions, fastening, material direction, worktable access, and repeat stops determine the useful press configuration.
Manual or matched feeding, discharge, part handling, and inspection flow should be reviewed with the output target.
Guarding, control mode, access, service space, and safety procedure are confirmed before operation.
CONFIGURATION POINTS
Provide die drawing, blank or strip direction, stages, shut height, required force calculation, and expected work position.
Confirm material grade, thickness, coil or blank format, finished geometry, edge condition, and tolerances.
Define feed method, target output, loading, discharge, inspection, guarding, and operator method.
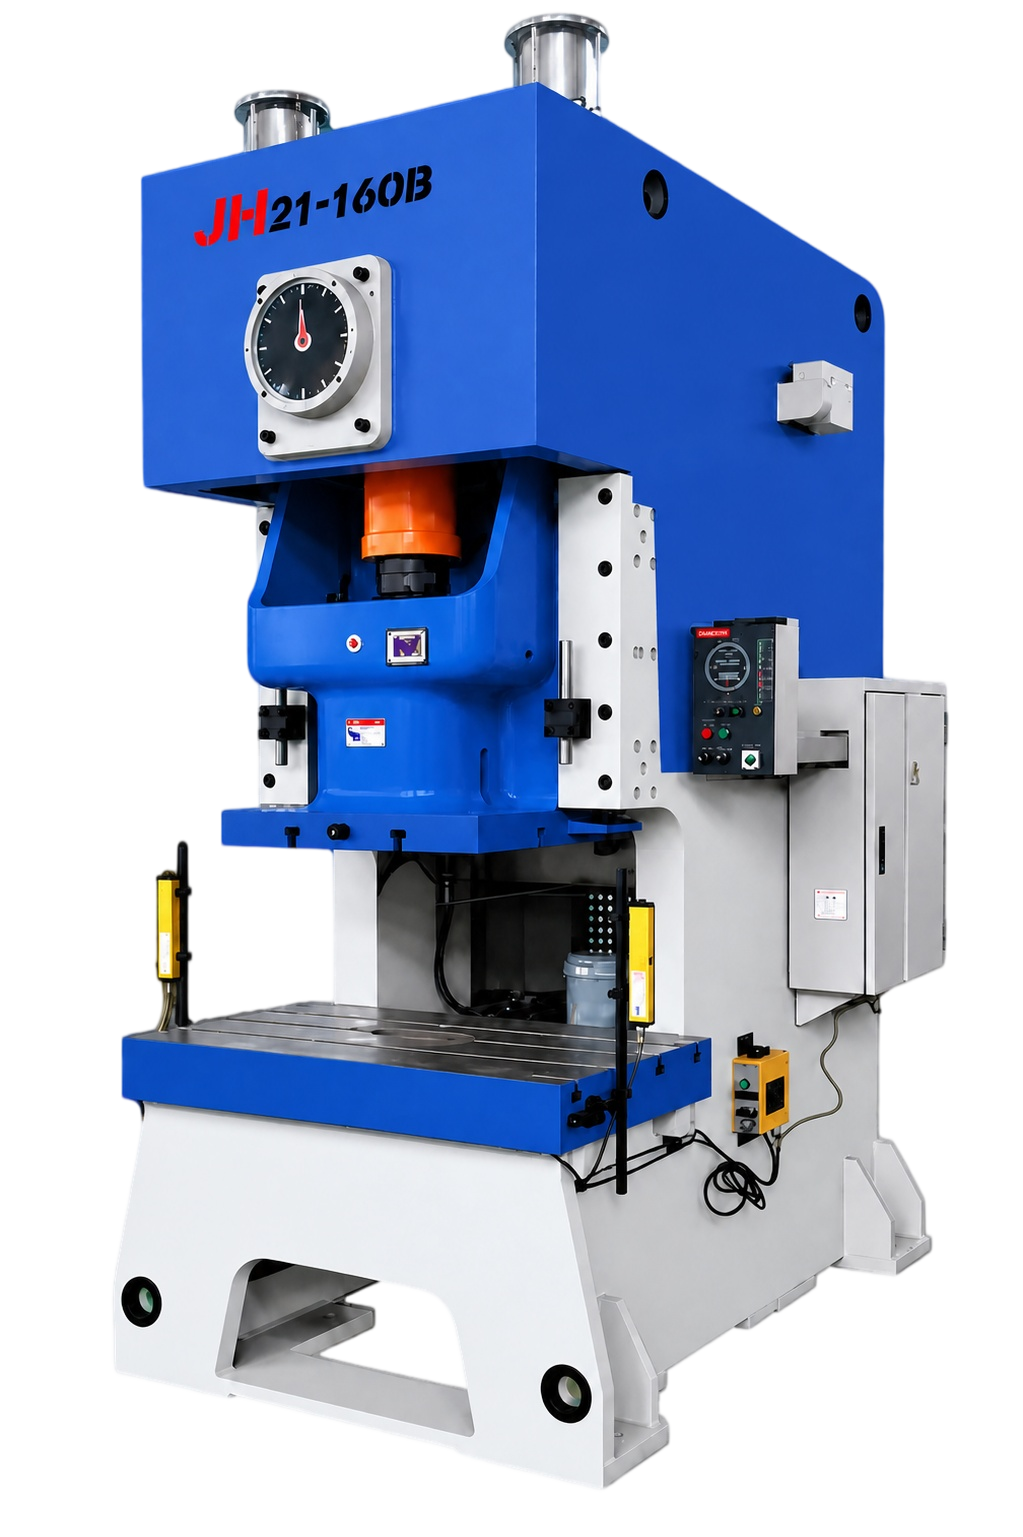
The product image is a JH21-160B reference only and does not establish equivalence with JH21-160. Fixed and variable stroke rates are separate values; final tooling and configuration are confirmed in the technical agreement.
| Technical parameter | Code | Unit | JH21-25 | JH21-45 | JH21-60 | JH21-80 | JH21-125 | JH21-160 | JH21-200 | JH21-250 | JH21-315 | JH21-400 |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Nominal capacity | Pe | kN | 250 | 450 | 600 | 800 | 1250 | 1600 | 2000 | 2500 | 3150 | 4000 |
| Nominal force travel | Sp | mm | 3 | 4 | 4 | 5 | 6 | 6 | 6 | 6 | 7 | 8 |
| Slide stroke | S | mm | 80 | 120 | 140 | 160 | 180 | 200 | 250 | 250 | 250 | 270 |
| Fixed slide strokes per minute | n | times/min | 100 | 80 | 70 | 60 | 50 | 45 | 45 | 30 | 30 | 30 |
| Variable slide strokes per minute | n | times/min | 60–100 | 50–80 | 45–70 | 40–60 | 35–50 | 30–45 | 25–45 | 20–30 | 20–30 | 20–30 |
| Maximum die set height | H2 | mm | 250 | 270 | 300 | 320 | 350 | 400 | 450 | 500 | 500 | 550 |
| Die height adjustment | t | mm | 50 | 60 | 70 | 80 | 90 | 100 | 110 | 120 | 120 | 120 |
| Throat depth | C1 | mm | 210 | 225 | 270 | 310 | 350 | 400 | 430 | 450 | 450 | 490 |
| Distance between uprights | d1 | mm | 450 | 515 | 560 | 610 | 670 | 736 | 910 | 980 | 980 | 1050 |
| Slide bottom size L–R | a | mm | 360 | 410 | 480 | 540 | 620 | 700 | 880 | 950 | 950 | 1020 |
| Slide bottom size F–B | b | mm | 250 | 340 | 400 | 460 | 520 | 580 | 650 | 700 | 700 | 750 |
| Die shank diameter | d | mm | 40 | 50 | 50 | 50 | 70 | 70 | 70 | 70 | 70 | 70 |
| Die shank depth | l | mm | 65 | 60 | 70 | 65 | 90 | 100 | 100 | 130 | 130 | 130 |
| Bolster size L–R | C | mm | 720 | 825 | 930 | 950 | 1100 | 1170 | 1390 | 1500 | 1540 | 1700 |
| Bolster size F–B | D | mm | 400 | 440 | 520 | 600 | 680 | 760 | 840 | 880 | 880 | 950 |
| Falling-hole diameter | φ | mm | 150 | 150 | 150 | 150 | 160 | 180 | 200 | 200 | 200 | 200 |
| Bolster thickness | H3 | mm | 80 | 110 | 130 | 140 | 155 | 165 | 180 | 190 | 190 | 210 |
| Bolster surface height | H1 | mm | 780 | 800 | 900 | 900 | 900 | 900 | 1000 | 1000 | 1000 | 1100 |
| Overall dimensions L–R | A | mm | 1496 | 1585 | 1540 | 1765 | 2040 | 2305 | 2600 | 2660 | 2720 | 2850 |
| Overall dimensions F–B | B | mm | 945 | 1075 | 1200 | 1200 | 1320 | 1420 | 1540 | 1640 | 1680 | 1750 |
| Overall dimensions H | H | mm | 2120 | 2391 | 2570 | 2725 | 3035 | 3215 | 3800 | 3865 | 3865 | 4150 |
| Foundation distance F–B | a | mm | 980 | 1075 | 1100 | 1210 | 1430 | 1665 | 2020 | 2100 | 2140 | 2260 |
| Foundation distance L–R | b | mm | 660 | 760 | 840 | 920 | 1040 | 1140 | 1840 | 1740 | 1810 | 1750 |
| Motor model | — | — | Y100L–4 | Y132S–4 | Y132S–4 | Y132M–4 | Y160M–4 | Y160L–4 | Y180M–4 | Y200L–6 | Y225M–6 | Y250M–6 |
| Motor power | — | kW | 3 | 5.5 | 5.5 | 7.5 | 11 | 15 | 18.5 | 22 | 30 | 37 |
| Approximate weight | — | kg | 2450 | 3550 | 5150 | 6450 | 9550 | 13600 | 19200 | 23200 | 26600 | 31600 |
TAILORED TECHNICAL PROPOSAL
Share drawings, materials, target output, and current process constraints. An engineer can use them to prepare the next conversation.