
Contents
- Chapter One: Start With Machine Compatibility
- Chapter Two: Define the Material and the Production Conditions
- Chapter Three: Comparing the Four Common Blade Materials
- Chapter Four: Blade Geometry, Clearance and Rake Angle
- Chapter Five: Ordering Replacement Blades and What to Send
- Chapter Six: Comparing Shear Blade Suppliers
- Chapter Seven: The Real Number, Cost per Cut
- Chapter Eight: Putting the Blade Back into the Machine, the GWMT QC11Y/K Shearing Series
- Frequently Asked Questions
- Conclusion
The sentence you hear most often about shear blades in a workshop is "just order the same set again". Sometimes that is right. More often it simply means nobody wrote down what actually mattered. What material and what thickness was the last set cutting? Was it bought because it was cheap, or because that job genuinely needed a grade that resists chipping? If those answers were never recorded, the next blade selection is a guess. This guide does something else: it turns blade selection from an act of experience into a decision path you can walk end to end.
Choosing the wrong blade rarely produces an immediate failure. What it produces is shorter-than-expected service life, inconsistent cut quality, or chipping that appears before the edge has seen real wear. These three symptoms have entirely different causes and entirely different remedies: some need a different material, some need a different clearance, some need better alignment. Treating them as one problem usually ends with an expensive blade that does not fix anything. Correct selection matches the blade to the machine, the material and the production conditions at the same time, rather than repeating the nominal size of the last set.
This guide covers the parts of hydraulic shear blade selection that actually decide the outcome: machine compatibility, blade material, blade geometry, the information a supplier needs in order to quote accurately, and how to compare options on cost per cut rather than on purchase price.
1. Chapter One: Start With Machine Compatibility
Before comparing blade grades or contacting suppliers, confirm that the blade you are considering is approved for the machine. Physical fit, meaning matching holder length and bolt pattern, is necessary but not sufficient.
What you need is the machine documentation, not a sales catalogue.
- Exact machine model and serial number, not the product family or nominal capacity class
- Shear design: hydraulic guillotine, swing-beam or another configuration
- The approved blade part number or drawing reference from the machine manufacturer
- Rated capacity, verified against the actual material grade, tensile strength and cutting length. A capacity figure based on mild steel does not apply to high-strength structural plate.
- A different blade material does not increase the machine rated capacity. If the workpiece or cutting length falls outside what the documentation covers, contact the machine manufacturer before ordering.
1.1 1.1 Verify the Blade Drawing
Nominal blade dimensions, meaning length, width and thickness, are not a complete specification. The drawing governs the details that decide whether the blade seats correctly and cuts accurately.
- Bevel angle and direction: the slope of the cutting face must match the blade holder geometry
- Hole pattern: centre distances, hole diameters and countersink angles and depths
- Mounting orientation: which face seats against the holder and which edge is in the cutting position
- Tolerances: dimensional tolerances matter for seating, fastener engagement and edge position
- If you are measuring from an existing blade, treat those measurements as a cross-check, not the sole specification. Previous regrinding may have reduced thickness or altered edge geometry. Resolve any discrepancy against the approved drawing before ordering.
1.2 1.2 Confirm the Upper and Lower Blade Configuration
Upper and lower blades are not always interchangeable. Identify each position separately when ordering.
- Single-edge or reversible: if the blade can be rotated, confirm how many edges are actually usable in the permitted mounting positions on your machine. Not every corner qualifies.
- One-piece or segmented: segmented arrangements can simplify handling where permitted, but joint positions must match the machine design
- Individual replacement or matched set: on some machines, replacing a single blade without matching the remaining blades introduces seating or alignment inconsistencies
- These are machine-specific requirements, not optional preferences.
2. Chapter Two: Define the Material and the Production Conditions
Blade selection begins with a clear description of the actual work, not a general category. "We cut steel" covers too wide a range to support a useful recommendation.
Document the following before contacting a supplier.
- Material family: carbon steel, stainless steel, aluminium, galvanised or coated sheet, high-strength structural steel
- Material grade and specified tensile strength, where available
- Thickness range: minimum, maximum and the combination most common in daily production
- Maximum cutting length
- Surface condition: scale, coatings or surface treatments that affect abrasiveness and wear behaviour
- Production volume: cuts per shift, batch patterns and whether the machine runs continuously or intermittently
- Cut-quality requirements: acceptable burr height, edge straightness and dimensional tolerance
- The combination that drives the most wear, chipping or quality complaints in your current production, not the average case, is the one the blade must handle reliably. A blade selected for average conditions often fails at the demanding end of the range.
3. Chapter Three: Comparing the Four Common Blade Materials
For hydraulic guillotine shearing of sheet metal and plate, most applications are served by a small set of tool steel grades. Each represents a different balance of wear resistance, toughness and suitability for the operating conditions.
The table describes general tendencies, not absolute rankings. Heat treatment, specified hardness range and manufacturing quality within the same nominal grade can affect performance significantly. A material certificate with documented hardness and heat-treatment traceability is more informative than a grade name alone.
Other tool steels, including A2, 5160, M2 high-speed steel and carbide-tipped designs, are used in specialised industrial shearing applications, but they are not standard choices for most hydraulic sheet-metal guillotine shears.
| Blade material | Wear resistance | Toughness | Typical applications |
|---|---|---|---|
| 9CrSi | Medium | Medium | General sheet metal, mild and carbon steel, cost-effective general use |
| D2 / SKD11 / Cr12MoV-type | High | Medium | Stainless steel, coated sheet, higher production volume, abrasive materials |
| 6CrW2Si | Medium to high | High | Heavy-duty cold shearing, thicker plate, applications with higher impact loading |
| H13 | Medium | High, thermal | Hot shearing or applications involving elevated blade temperature |
3.1 3.1 9CrSi: General-Purpose Sheet Metal Cutting
9CrSi is the most widely used blade steel for hydraulic guillotine shears on carbon steel and mild steel. It offers a practical balance of wear resistance, toughness and cost, and is widely available in standard and custom blade dimensions. It is a reasonable starting point for shops cutting a mixed range of materials and thicknesses at moderate production volume.
3.2 3.2 The D2 / SKD11 / Cr12MoV Group: Stainless Steel and High-Volume Work
High-chromium tool steels in the D2 / SKD11 / Cr12MoV group are commonly recommended for stainless steel, galvanised sheet, coated materials and operations where gradual edge wear is the primary service-life limit. Their high carbon and chromium content provides substantially better abrasion resistance than 9CrSi.
The trade-off is toughness. These grades are more susceptible to chipping than 9CrSi or 6CrW2Si when clearance is incorrect, alignment is imperfect or the material feed is inconsistent. Upgrading to a D2-type grade does not compensate for a setup problem. If blades are chipping rather than wearing, review clearance and alignment before changing the blade material.
Note that D2 (AISI), SKD11 (JIS) and Cr12MoV (GB) are different designations from different standards systems. Although they share a similar high-chromium, high-carbon composition, they are not identical. Specify the standard and grade designation clearly when ordering rather than using the terms interchangeably.
3.3 3.3 6CrW2Si: Heavy-Duty Cold Shearing
6CrW2Si offers higher toughness than D2-type grades while retaining reasonable wear resistance. It is used in applications involving thicker plate, higher impact loading, or conditions where chipping has been a persistent problem with harder grades.
3.4 3.4 H13: Hot Shearing Applications
H13 is a hot-work die steel that maintains hardness and resists thermal fatigue at elevated temperatures. Its relevance is specific: it is appropriate where blade temperature is a material factor, such as in hot shearing of heated plate. For standard room-temperature hydraulic sheet-metal shearing, the lower hardness of H13 compared to D2-type grades provides no advantage and is not a typical selection.
4. Chapter Four: Blade Geometry, Clearance and Rake Angle
Beyond steel grade, blade geometry affects how the cut progresses and how load is distributed across the cutting edge. The three parameters in this chapter each explain a large class of problems on the shop floor.
- Bevel angle at the cutting edge influences edge strength and cutting force. A sharper, lower-angle edge reduces cutting force and produces a cleaner cut on thin or soft materials. A stronger, higher-angle edge handles thicker or harder materials more reliably but requires more force. Blade drawings specify the approved bevel: do not assume the geometry from a previous blade applies if the grade or supplier has changed.
- Clearance is the gap between the upper and lower cutting edges. Many sheet-metal applications fall within roughly 5–10% of material thickness as a general reference, but the machine manufacturer clearance chart takes priority over any general rule. Incorrect clearance is one of the most common causes of excessive burrs, edge deformation and premature blade wear.
- Rake angle is primarily determined by the shear mechanical design and cutting configuration. It affects cutting-force distribution and material distortion across the cut length, but operators should follow the machine manufacturer specified setting rather than treating rake angle as a general adjustment variable.
5. Chapter Five: Ordering Replacement Blades and What to Send
Ordering replacement blades is where specification errors most often occur. The information below is what a supplier needs in order to quote accurately and supply a compatible blade.
- Machine and blade identification: machine model, serial number and shear design; the approved blade part number or drawing reference, providing the drawing rather than measurements from a worn blade; the upper or lower position, specified separately for each
- Application details: material grades and specified strength; thickness range covering minimum, maximum and typical; maximum cutting length; production volume and duty cycle
- Documentation requirements: steel grade designation and applicable standard, whether AISI, JIS, GB or equivalent; specified hardness range in HRC and heat-treatment condition; a material certificate or mill certificate traceable to the supplied blades; a dimensional inspection report confirming hole pattern, bevel geometry and tolerances
- Practical steps before bulk ordering: request a trial set for a new grade or new supplier before committing to full quantity; run trial cuts on the actual material and thickness range used in production; inspect cut quality including burr level, edge squareness and distortion; record cutting conditions, edge condition at the start of service and any anomalies
- A supplier who can explain why the proposed grade and heat treatment suit your specific application, with reference to your machine and material, is more useful than one who defaults to their most-sold product.
6. Chapter Six: Comparing Shear Blade Suppliers
Blade sourcing decisions made on unit price alone frequently produce higher total operating cost. Evaluation should cover three areas.
- Technical capability: can the supplier confirm grade, heat treatment and hardness documentation for each supply? Do they offer blades ground to the machine-approved drawing rather than standard sizes only? Can they provide material certificates and dimensional inspection records?
- Service and support: what are standard lead times for custom-dimensioned blades? Do they offer regrinding services within specified geometry and minimum dimension limits? Can they supply matched sets when the machine requires it?
- Supply reliability: is the grade you need consistently available, or subject to extended lead times? What is the minimum order quantity for custom specifications?
- A supplier with long lead times on a critical blade grade creates inventory and production risk that does not appear in the quoted price.
7. Chapter Seven: The Real Number, Cost per Cut
The lowest-priced blade is rarely the lowest-cost choice over a production cycle. A more useful comparison accounts for the following.
- Usable cutting edges before regrinding is required
- Regrinding cycles: how many times the blade can be reground within minimum dimension limits, and the cost and lead time per regrind
- Cutting volume per edge, based on actual material and duty
- Change-over time: labour and downtime for blade rotation, regrinding and full replacement
- Scrap and rework risk: blades producing marginal cut quality late in service generate cost that does not appear on the blade invoice
- Availability: a lower-unit-cost blade with long lead times creates inventory carrying cost and production exposure
8. Chapter Eight: Putting the Blade Back into the Machine, the GWMT QC11Y/K Shearing Series
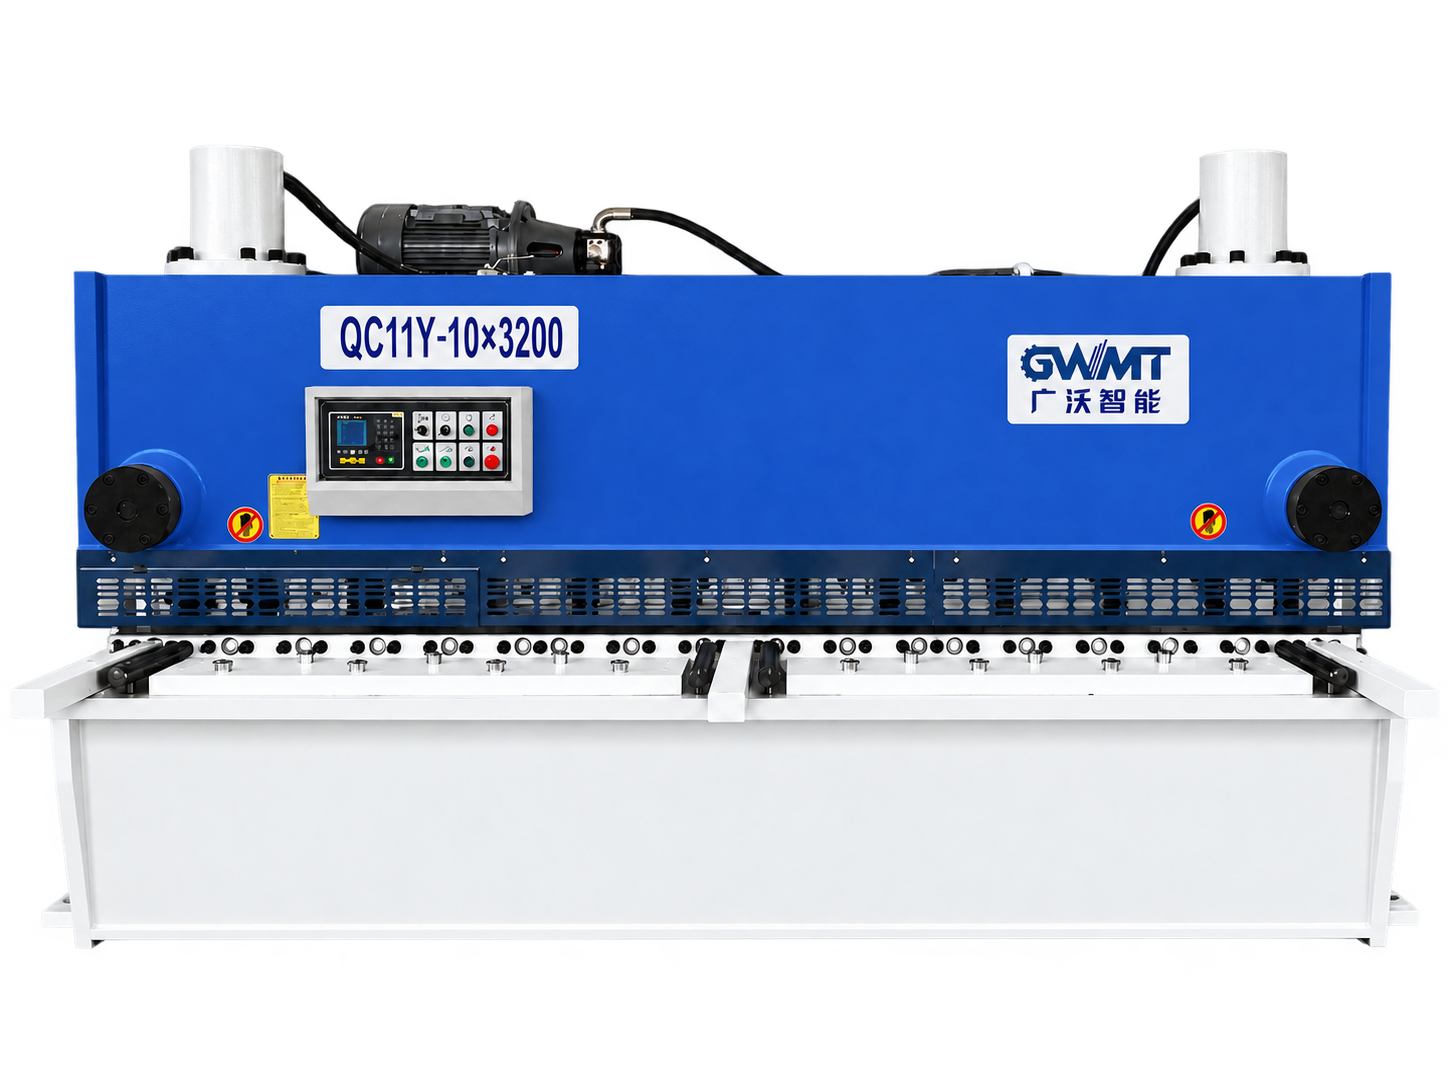
The previous seven chapters have been about the blade alone. What actually decides how long that blade lasts is how the machine it sits on works. A concrete example is the GWMT QC11Y/K hydraulic guillotine shearing series.
The QC11Y/K series covers capacities from 12 to 60 tonnes with cutting lengths from 2500 to 12000 mm. That spread matters on its own, because it means one machine may face a material range from thin sheet to medium plate. A shearing machine that mostly cuts 3 mm cold-rolled sheet and one that regularly cuts 12 mm plate need different blade strategies from the start.
In a specification like this, capacity and cutting length are only part of the story. Maximum cutting thickness, minimum cutting thickness and the maximum strokes per minute are all directly connected to blade selection. Maximum thickness sets the blade strength and the clearance baseline. Minimum thickness sets a limit in the other direction: too much clearance pushes thin sheet out of position instead of cutting it. Strokes per minute is cadence, and higher cadence means more cutting volume per hour and faster blade wear.
One practical selection point deserves a mention. In the QC11Y/K specifications, some capacities list a minimum cutting thickness clearly below their neighbours: in the 20 tonne series, for example, the 12000 mm machine is listed at 3–12 mm while the 8000 mm machine reads 4–15 mm. If you are choosing between the two and your order book carries a lot of thin work, the minimum cutting thickness may matter more than you expect. A machine with a higher nominal capacity but a larger minimum thickness is not automatically the better choice in production.
It is worth being clear that these are reference dimensions for asking the right questions during selection, not a confirmed configuration commitment for any particular machine. Actual capability, the approved blade list and the matching items are confirmed in the technical proposal for the specific duty.
- Putting the blade question back into the machine specification: when you evaluate a new shearing machine, asking for its approved blade list and the recommended blade grade is part of the selection. A machine with a stable blade supply, a clear drawing and easily sourced spares often works out cheaper over two years of production than one with a prettier specification sheet.
- If you are specifying a shearing machine for a new line, or trying to trace why blades wear out quickly on an existing one, the three most useful questions are these: which blades does this machine approve, what does the machine clearance chart give for this material and thickness, and is the current grade too soft or too hard for the actual duty. These three questions describe the machine far better than any claim about accuracy class.
9. Frequently Asked Questions
The six questions below suit item-by-item confirmation with a customer, a colleague or a supplier.
- How do I identify the correct replacement shear blade for my machine?
Start with the machine model, serial number and service documentation to locate the approved blade part number or drawing. The drawing specifies dimensions, bevel geometry, hole pattern, countersinks and mounting orientation. Do not rely on measurements from a worn blade alone, because previous regrinding may have changed critical dimensions.
- What is the best blade material for cutting stainless steel?
D2-type high-chromium tool steels, the D2 / SKD11 / Cr12MoV group, are the standard recommendation for stainless steel and coated sheet. Their high wear resistance suits the abrasive nature of stainless and the work-hardening behaviour it exhibits under shearing. Confirm machine compatibility and clearance settings before upgrading from a general-purpose grade: chipping problems are more likely to be caused by clearance or alignment issues than by the blade material.
- Is D2 always the best shear blade material?
Not always. D2-type grades offer high wear resistance but moderate toughness. If blades are chipping rather than wearing, which is often a sign of incorrect clearance, misalignment or inconsistent material feed, a tougher grade such as 6CrW2Si may outlast D2 in practice even if D2 looks better on paper. Identify whether wear or chipping is the failure mode before selecting a replacement grade.
- Why do new shear blades still produce burrs?
Burrs are most commonly caused by incorrect clearance, improper blade seating or misalignment, not a defective blade. Check clearance against the machine manufacturer chart for the actual material and thickness. Verify blade seating, fastener torque and alignment along the full cutting length before concluding that the blade is at fault.
- When should a shear blade be reground or replaced?
Regrind when edge wear is progressing but the blade has not suffered chipping or cracking: early regrinding removes less material and preserves more service cycles. Replace when the blade is cracked, chipped beyond regrinding, or has reached the minimum allowable dimension after repeated grinds. Do not rotate a chipped edge into the cutting position.
- What information should I provide when ordering custom shear blades?
Provide the machine model and serial number, the approved blade drawing or part number, the upper or lower blade position, material grades and tensile strength, thickness range, cutting length, production volume and any known problems with the current blade. Also request the steel grade designation, the heat-treatment specification, hardness documentation and a material certificate traceable to the supplied blades.
10. Conclusion
Shear blade selection comes down to four decisions made in the right order: confirm machine and drawing compatibility, define the actual material and production conditions, choose blade material and geometry to match, and validate performance with trial cuts before full production.
The most common selection mistakes, ordering by price, skipping the blade drawing, or upgrading to a harder grade without diagnosing whether chipping or wear is the real failure mode, all become less likely when the selection process follows that sequence.
One more point deserves separate mention: the blade service record is itself an asset. Logging material, cutting volume, regrind dates and defects gives you your own basis for comparison instead of relying on supplier estimates. If no record is being kept today, starting one with the next blade set produces real data within a few months of production.
If you are specifying a hydraulic shearing machine for a new line, or trying to trace the root of a short blade life on existing equipment, gathering the machine model, blade drawing reference, material specification and thickness range is enough to turn "which blade should I use" into a question that can be answered.
Technical references
Manufacturer references support process explanations; images illustrate selection topics, not an approved GWMT supply specification.