استفسارات المنتجات

المعرفة الصناعية

مركز الأخبار/المعرفة الصناعية

22 مقالات

أقصى عزم انحناء: الصيغ والأمثلة المحسوبة والحكم الهندسيالمعرفة الصناعية

أقصى عزم انحناء: الصيغ والأمثلة المحسوبة والحكم الهندسي

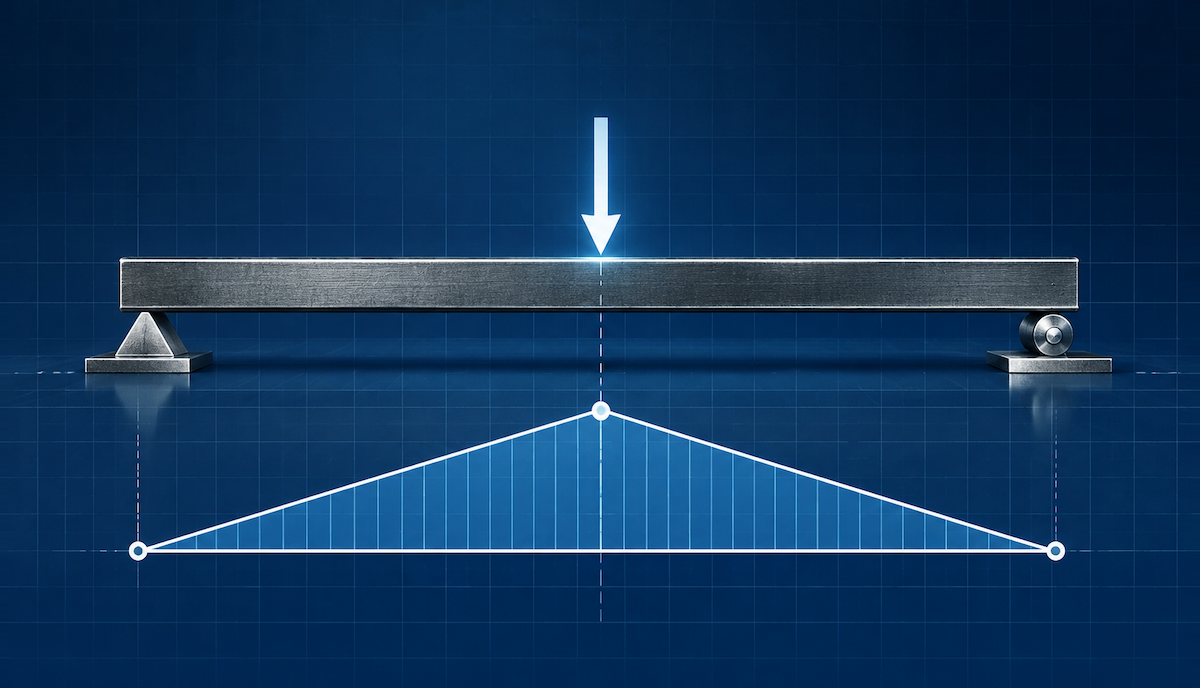
أقصى عزم انحناء هو أحد أول الأرقام التي يلجأ إليها المهندس — فهو يحدد الحد الأدنى لاختيار مقطع المقطع، ويوجه اختيار الخامة، ويحدد كيف تُخطَّط سعة الآلة، وكل قرار لاحق يرث الخطأ إن كان الخطأ قد وقع. ويسترشد هذا الدليل عبر مسار الحساب كاملًا: ما هو عزم الانحناء ميكانيكيًا في الحقيقة؛ وحقيقة أن "maximum" تشير إلى رقمين مختلفين؛ ولماذا يجب تثبيت حالة الدعامة والحمل أولًا؛ وأربع خطوات لإيجاد القيمة العظمى؛ والصيغ الخمس التي تغطي معظم حالات الحساب اليدوي مع مثالين محسوبين كاملين؛ وكيف تنقل النتيجة إلى فحص إجهاد الثني. كما يوضح الدليل أيضًا أكثر ما يُساء استخدامه: عزم التسييل الأول لكمرة إنشائية ليس سعة تشكيل في مكبس ثني الصفائح. ويُحفظ كلٌّ من الجدولين المصدرين وكل صيغة وكل رقم كما نُشرت.

اقرأ المزيد
سلامة مكبس ثني الصفائح: ⁦12⁩ خطرا وحواجز الحماية ومتطلبات OSHAالمعرفة الصناعية

سلامة مكبس ثني الصفائح: ⁦12⁩ خطرا وحواجز الحماية ومتطلبات OSHA

يمكن لمكبس ثني الصفائح أن يغلق بقوة تكفي لسحق العظم في جزء من الثانية، وغالبا ما لا تكون يدا المشغل إلا على بعد بضعة سنتيمترات من فجوة الإغلاق تلك. ففي مكبس ثني الصفائح، تقع منطقة الخطر ومنطقة العمل في المكان نفسه. يفكك هذا الدليل ⁦12⁩ خطرا تقف وراء معظم إصابات مكابس ثني الصفائح، ويعرض الممارسات اليومية التي تقي منها، ويشرح كيف تعمل الستائر الضوئية والحماية الليزرية فعليا، وأين تقصر حواجز الحماية والتحكم باليدين عن توفير الوقاية الكاملة، وما تشترطه OSHA وANSI وEN وISO، ويقدم قائمة تحقق يمكن لمشغليك تنفيذها في كل وردية. ويتم الإبقاء على جدولي المقارنة وكل أرقام المعايير بصيغتها المنشورة.

اقرأ المزيد
أدوات التشكيل لمكبس ثني الصفائح في الثني الهوائي والثني حتى قاع القالب والثني بالسك: دليل كاملالمعرفة الصناعية

أدوات التشكيل لمكبس ثني الصفائح في الثني الهوائي والثني حتى قاع القالب والثني بالسك: دليل كامل

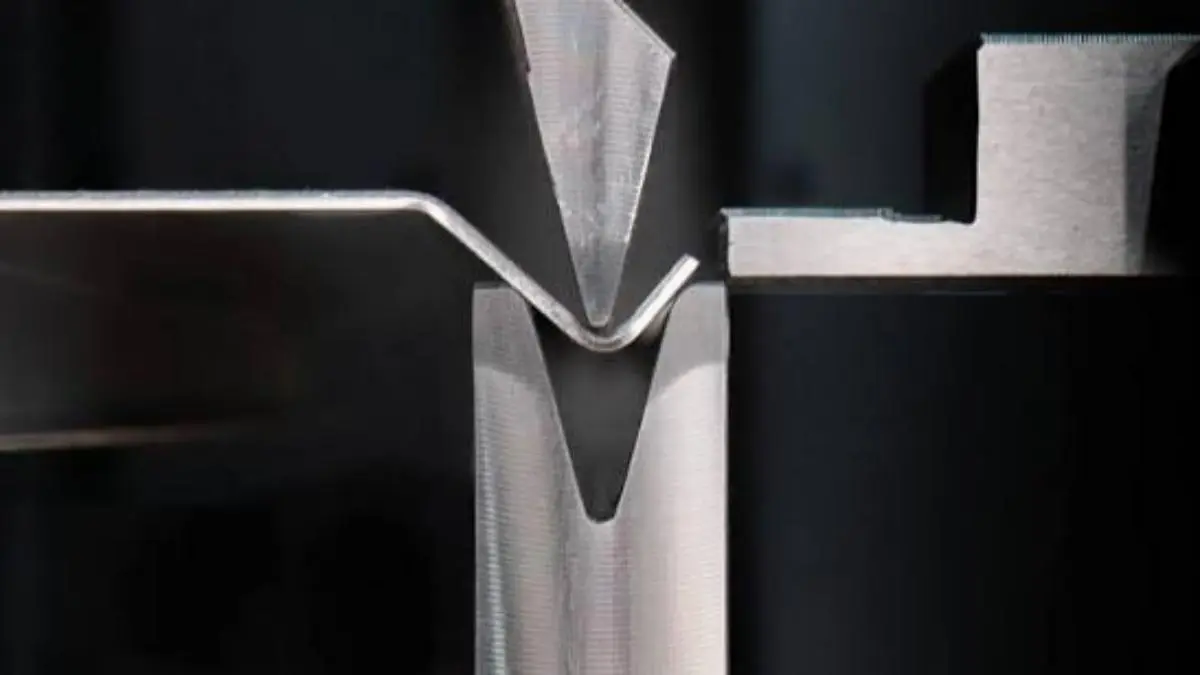
Air bending, bottoming and coining get used interchangeably on the shop floor, but they are three different processes and they need three different sets of tooling. Choose wrongly and the angle drifts, the tooling dies early and the sheet cracks — and none of that is the machine's fault. It starts with mixing up the method. This guide takes the three apart one at a time: how the tooling works in each, what it demands, how to select it, how to manage springback, how the machine type changes the picture, and the five mistakes that cost the most.

اقرأ المزيد
مشكلات جودة القطع بالليزر: عالج السبب قبل أن تزيد القدرةالمعرفة الصناعية

مشكلات جودة القطع بالليزر: عالج السبب قبل أن تزيد القدرة

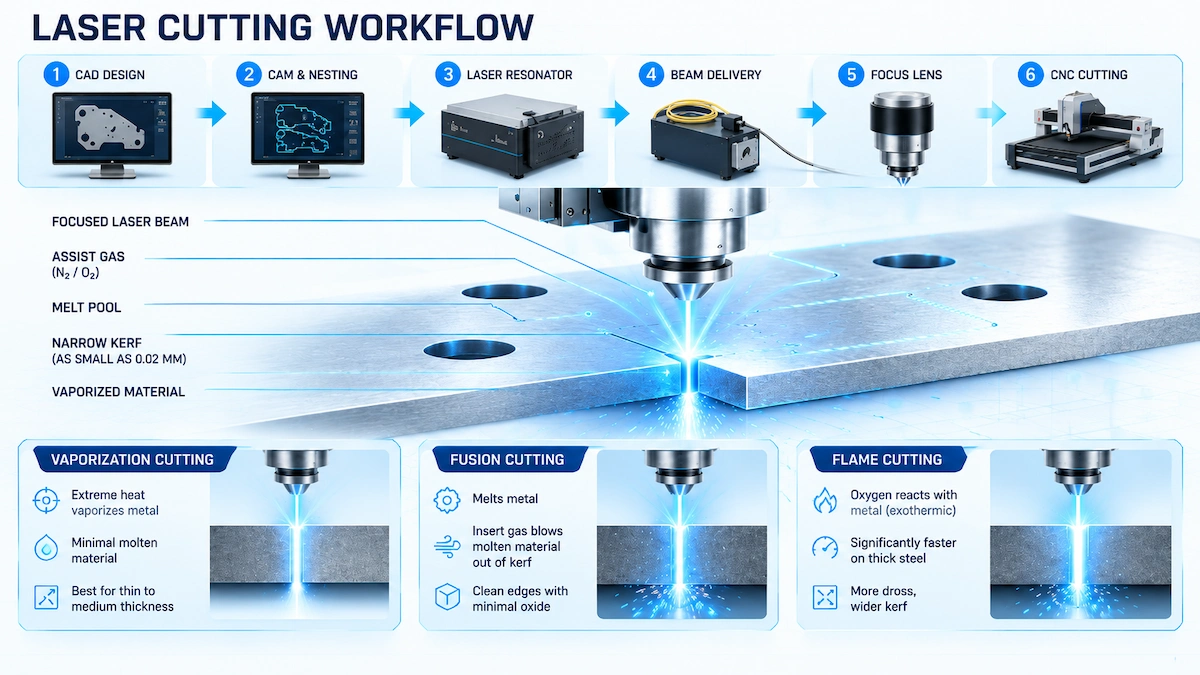
Incomplete cuts, bottom dross, a kerf that is too wide, dross on one side only, burned sharp corners and dimensions that drift: all of these happen every day on the shop floor, and the first reaction in most cases is to add power. Cut quality is never decided by a single parameter. It is the combined result of how laser energy is focused, absorbed by the material and cleared by the assist gas, plus how the machine moves, how the part is programmed and how stable the environment is. This guide takes that chain apart into nine variables, each with what to check first, what to check next and why, and keeps the source seven-row troubleshooting table unchanged so you can work back from the symptom instead of guessing at parameters. Nine chapters cover the physical chain a cut follows, the beam and the focus, gas and nozzle, motion and maintenance, programming and environment, and the guide closes with two points about applying the method to a GWMT machine: published figures are reference ranges rather than a rated commitment, and buying a machine and running it well are two different things.

اقرأ المزيد
كيفية اختيار شفرات القص لماكينات القص الهيدروليكية: درجة الفولاذ والهندسة والطلب والتكلفة لكل قطعة مقطوعةالمعرفة الصناعية

كيفية اختيار شفرات القص لماكينات القص الهيدروليكية: درجة الفولاذ والهندسة والطلب والتكلفة لكل قطعة مقطوعة

تكلفة مجموعة الشفرات الاحتياطية أقل بكثير من ماكينة قص جديدة، لكن تكلفة الاختيار الخطأ غير ظاهرة: فالشفرات لا تتعطل عند أول قطعة مقطوعة، بل تتزايد البرادة ويظهر تكسّر الحافة مبكرًا وتدوم الشفرة مدة أقصر بوضوح مما ينبغي. وتشتري ورش كثيرة الحجم الاسمي نفسه الذي كانت عليه المجموعة السابقة، فتنتهي باستهلاك الشفرات أسرع مما تستحقه الماكينة. يقسّم هذا الدليل قرار الاختيار إلى أربع خطوات يجب اتخاذها بالترتيب: التحقق من الشفرة التي تعتمدها الماكينة، ووصف نوع الخامة وظروف الإنتاج التي تقطعها فعليًا، واختيار درجة الفولاذ والهندسة بما يناسب ذلك العمل وطريقة تلف الشفرة، ثم التحقق من الاختيار بإجراء قطع تجريبي بدلًا من الاعتماد على التقدير الشخصي. وتُنقل مقارنة درجات فولاذ الشفرات الأربع الشائعة، ⁦9⁩CrSi وعائلة ⁦D2/SKD11/Cr12MoV⁩ و⁦6⁩CrW⁦2⁩Si و⁦H13⁩، كما هي، مع قائمة تحقق تغطي رسمة الماكينة وضبط خلوص القطع والتكلفة الحقيقية لكل قطعة مقطوعة.

اقرأ المزيد
صمام تناسبي لمكبس ثني الصفائح: مبدأ العمل والمزامنة وتشخيص الأعطالالمعرفة الصناعية

صمام تناسبي لمكبس ثني الصفائح: مبدأ العمل والمزامنة وتشخيص الأعطال

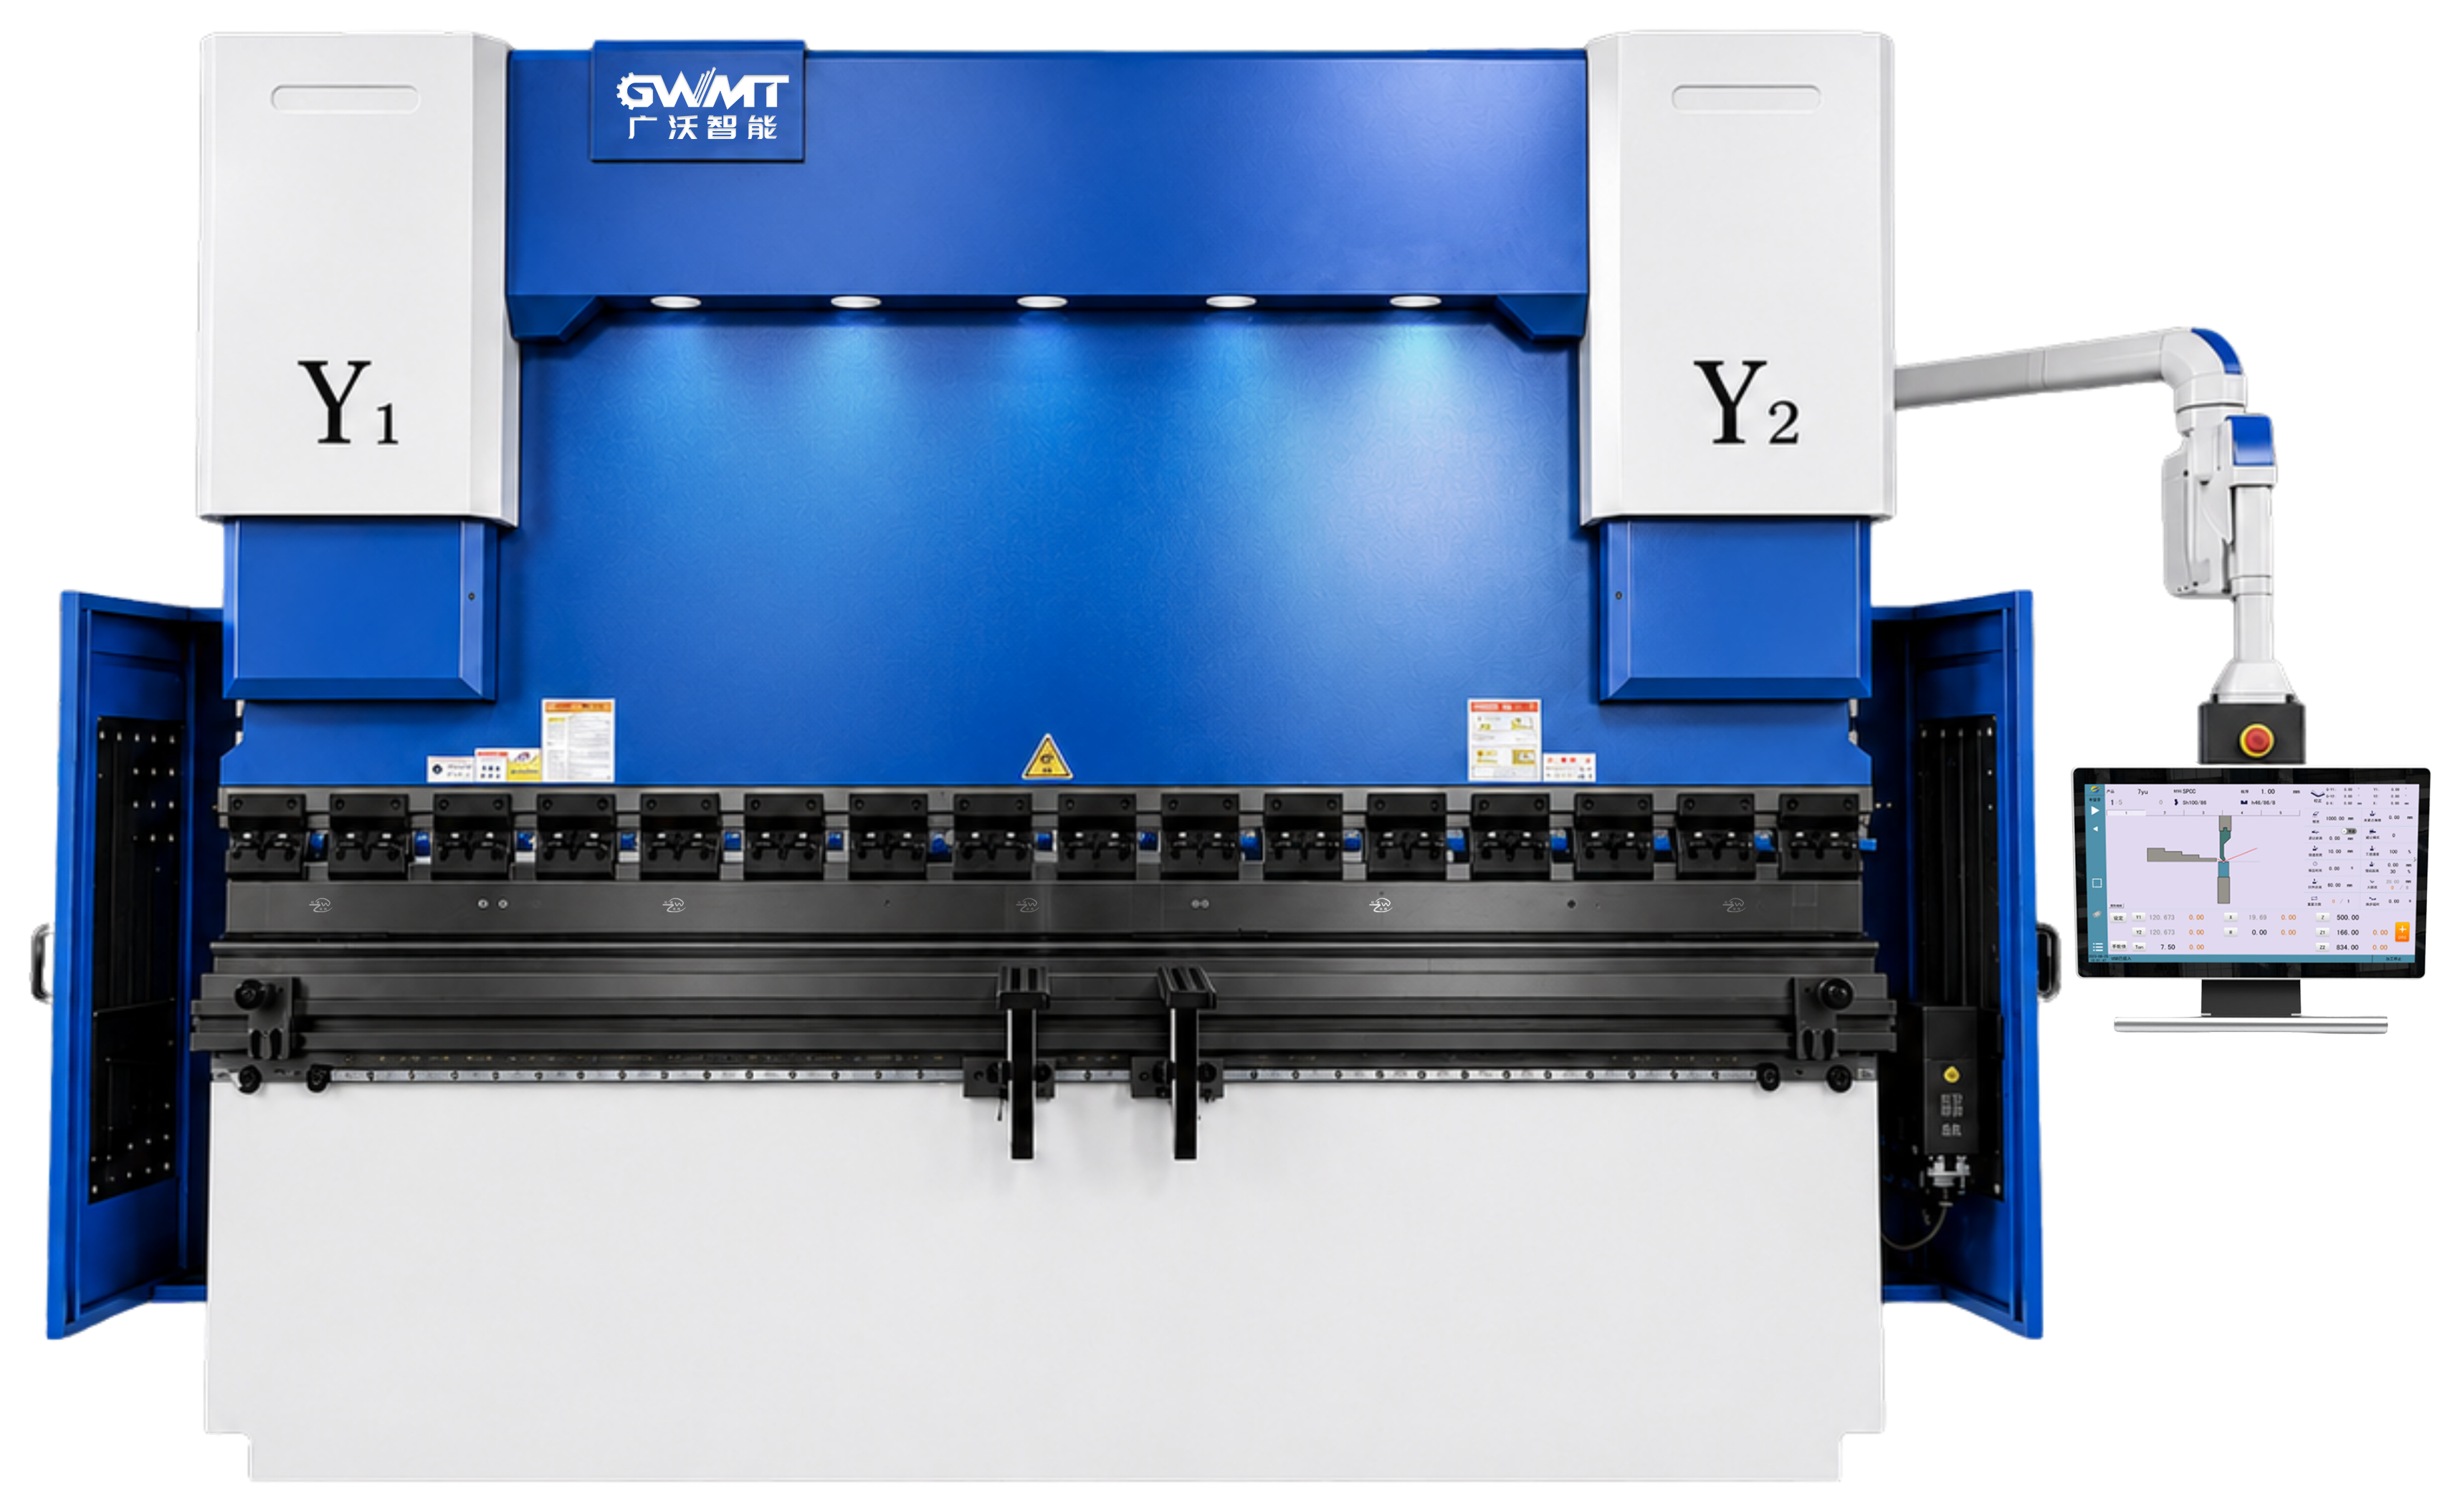
When the ram runs faster on the left than on the right, nine people out of ten will say the proportional valve has a problem. Get to the machine, open it up, and the valve is usually fine: the fault is somewhere else and only shows up as a synchronisation symptom. This guide takes that control chain apart in ten sections: what the proportional valve actually is, how an electrical signal becomes hydraulic flow step by step, what the valve opening is doing at each of the six phases of a bending cycle, how closed-loop Y1/Y2 synchronization keeps the ram parallel, where the real difference between proportional and servo valves lies, how to locate a fault at the correct system layer before anything is disassembled, the five parameter groups a replacement has to match, and whether the ram is safe once the power is off. All four source tables are kept in directly usable form: the two feedback types, torsion-bar against electro-hydraulic synchronization, proportional against servo valve characteristics, and the first-check order for six symptoms.

اقرأ المزيد
طرق الانحناء للصفائح المعدنية: ⁦11⁩ نوعًا من التشكيل والعوامل الأساسية وكيفية الاختيارالمعرفة الصناعية

طرق الانحناء للصفائح المعدنية: ⁦11⁩ نوعًا من التشكيل والعوامل الأساسية وكيفية الاختيار

The same 2 mm sheet steel can become a 90 degree bracket, a U channel, a hemmed sealing edge, a stepped offset, or a continuous curve. What decides which method applies is not habit but the part geometry, material and thickness, tolerance, appearance requirement and batch size. This guide sets out the full range of bending methods: the four basic forming modes of V bending, air bending, bottoming and coining, plus the seven dedicated methods of U bending, folding, wipe bending, roll bending, rotary bending, hemming and offset bending. All three source tables, the eleven-method quick reference, the part-scenario mapping and the machine-per-method table, are kept in directly usable form, together with a set of checks to run before releasing a bending drawing.

اقرأ المزيد
تشغيل ماكينة القطع بالليزر: دليل من عشر خطواتالمعرفة الصناعية

تشغيل ماكينة القطع بالليزر: دليل من عشر خطوات

A laser cutting machine can produce thousands of dimensionally identical parts, or it can scrap a full job in its first work order because one startup step was out of order, the focus was off by half a millimetre or the first article was never inspected. This guide breaks the complete operating sequence into ten stages: safety and readiness, startup and homing, CAD/CAM and toolpath, loading and job origin, head calibration, trial cut and first article, production monitoring, troubleshooting, shutdown and routine maintenance. Each stage states what to do first, what to check next, and the conditions that mean you stop and call for service. All three source tables, layer assignment, quick diagnosis and maintenance categories, are kept in directly usable form.

اقرأ المزيد
⁦15⁩ خطأً شاعيًا في مكبس ثني الصفائح: الأسباب والآثار والحلولالمعرفة الصناعية

⁦15⁩ خطأً شاعيًا في مكبس ثني الصفائح: الأسباب والآثار والحلول

One shift can turn out thousands of accurate bends and lose them again in minutes because of a few setup mistakes. This guide takes the fifteen most common press brake mistakes apart one by one: what the mistake is, why it happens, what it costs you in parts and money, and exactly how to put it right. From miscalculated tonnage and mismatched tooling to ignored springback, neglected crowning, backgauge drift, CNC programming, first-article inspection, hydraulic warnings and sheet handling, every section stands on its own for quick reference. All four reference tables are kept in directly usable form: material factors, what drives springback, typical springback and overbend values, and the maintenance interval schedule.

اقرأ المزيد
الدليل الكامل لمكبس ثني الصفائح: الأنواع ومبدأ العمل وحساب قوة الكبس والاختيارالمعرفة الصناعية

الدليل الكامل لمكبس ثني الصفائح: الأنواع ومبدأ العمل وحساب قوة الكبس والاختيار

A press brake is the machine that puts a straight line into sheet metal, and it is the most flexible machine on the metalworking floor. This guide covers the whole picture in one place: how the five drive types differ, what every part from frame to backgauge actually does, the five steps of a bending cycle, how tonnage is estimated, how to answer the six selection questions, and the daily maintenance and safety baseline. The key specification list, the tonnage formula with its worked example and the quick match guide are given in directly usable form, and every chapter points to the deeper article that covers one topic in full.

اقرأ المزيد
اختيار قالب V لمكبس ثني الصفائح دون أخطاء: ثماني خطوات وثلاثة أمثلة محسوبة واستكشاف الأعطالالمعرفة الصناعية

اختيار قالب V لمكبس ثني الصفائح دون أخطاء: ثماني خطوات وثلاثة أمثلة محسوبة واستكشاف الأعطال

Whether one opening produces acceptable parts depends on whether you check all eight constraints together. This guide turns V-die selection into an executable workflow: fix the bending method, take the starting range for your material, then verify tonnage, inside radius, minimum flange, springback consistency and surface quality before you settle on a slot width, trial bend and record the result. Three worked examples are included - 3 mm mild steel, 3 mm stainless steel and 2 mm aluminium - together with how to work a four-way die, how to diagnose six typical faults, and how to inspect, maintain and store the tooling.

اقرأ المزيد
كيفية اختيار فتحة قالب V لمكبس ثني الصفائح: جدول وقاعدة ⁦8⁩المعرفة الصناعية

كيفية اختيار فتحة قالب V لمكبس ثني الصفائح: جدول وقاعدة ⁦8⁩

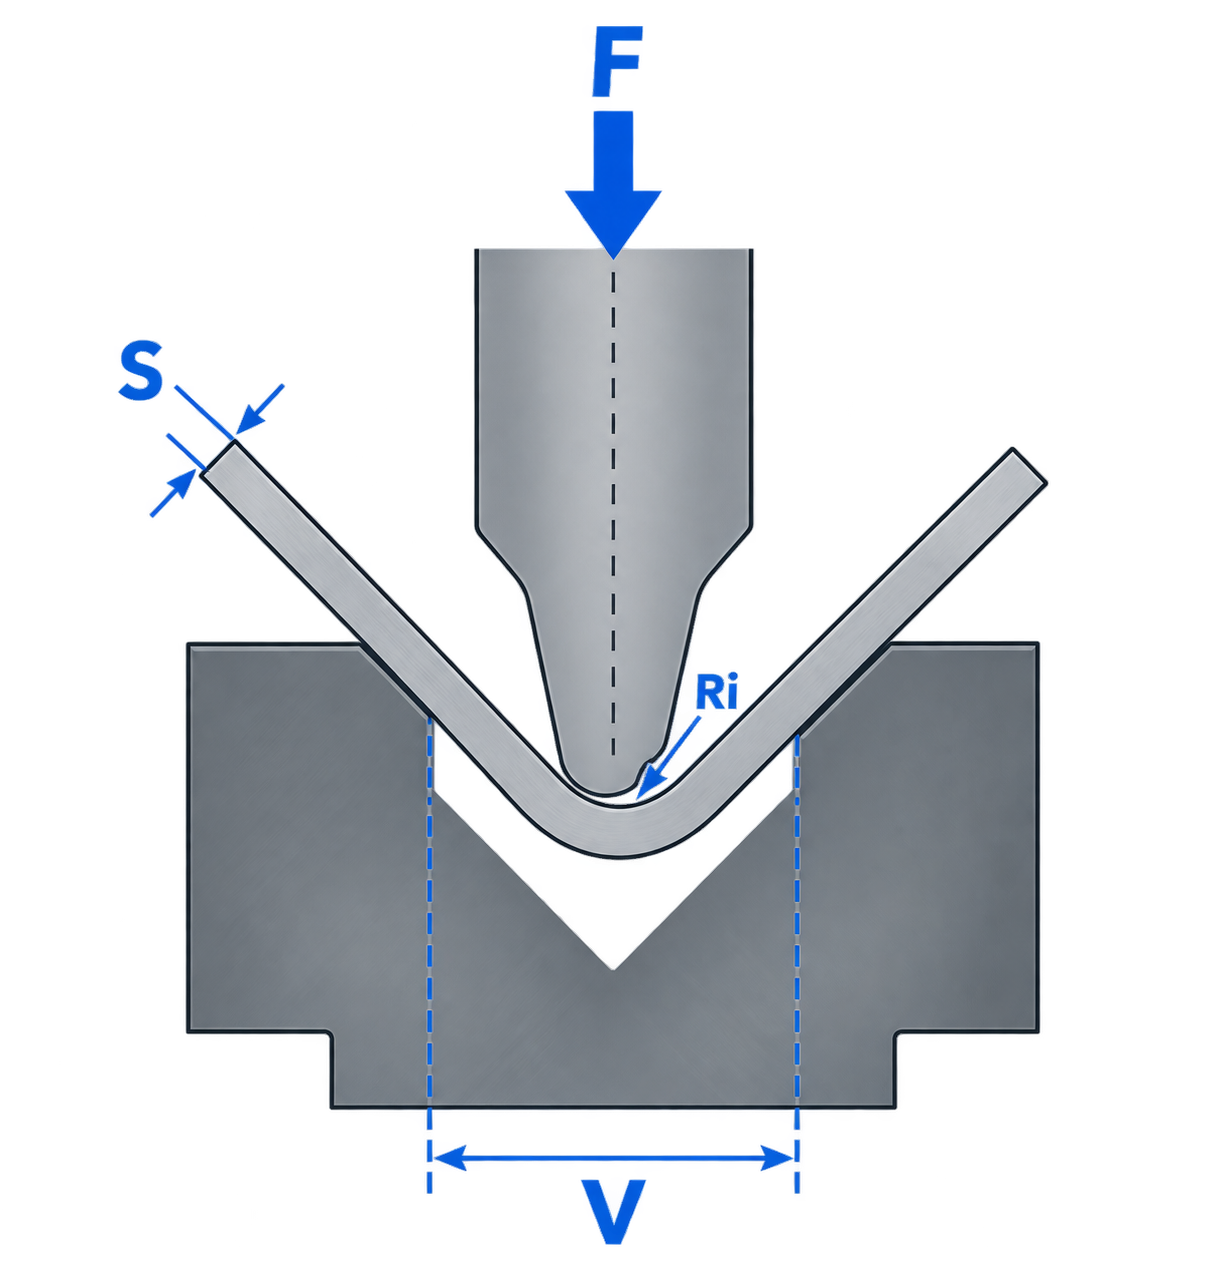
A V opening is not a groove width you pick by feel: it settles the inside radius, the tonnage your press brake must deliver and the shortest flange you can form, all at once. This guide gives a lookup chart for V openings, the Rule of 8 with its material corrections, the 16 % relationship between opening and radius, the tonnage formula with two safety checks, the 0.77 × V minimum flange rule, a five-step selection workflow and the four mistakes that cost the most time.

اقرأ المزيد